In this module, we will discuss the final stage of case studies – sharing or reporting of your case study.
Many business problems (complex, with breadth and depth) warranting a case study that a single
holistic case cannot address on its own. A Lean Six Sigma integrated Multiple-Case Case Study is just
the business solution because generally these cases will require some quantitative or mixed methods
elements. Use the excellent case presented in the Zhang et al. (2015) article as a model for your
multiple-case case study. After reviewing the Reading & Study material for the module, address the
following paper in current APA format:
1. Define the case study report audience and the appropriate reporting methodology
2. Compose visual and textual materials of a case study report
3. Explain the appropriate amount of evidence to present to facilitate the reader’s own conclusions to a
case study
4. Design a multiple-case case study that while covering multiple cases still draws a single set of cross-
case conclusions (single large organization, not multi-organizational). You will include Lean Six Sigma
specifically in the Design (type 4), Collect and Analysis (cross-case synthesis) phases of your case
study (use the Zhang et al. (2015) article as a model). [Also see Boxes 3, 32, and 38 (Yin, 2018)]
BUSI 830
MULTIPLE-CASE CASE STUDY ASSIGNMENT INSTRUCTIONS
In this module, we will discuss the final stage of case studies – sharing or reporting of
your case study. Many business problems (complex, with breadth and depth) warranting a case
study that a single holistic case cannot address on its own. A Lean Six Sigma integrated
Multiple-Case Case Study is just the business solution because generally these cases will require
some quantitative or mixed methods elements. Use the excellent case presented in the Zhang et
al. (2015) article as a model for your multiple-case case study. After reviewing the Reading &
Study material for the module, address the following paper in current APA format:
1. Define the case study report audience and the appropriate reporting methodology
2. Compose visual and textual materials of a case study report
3. Explain the appropriate amount of evidence to present to facilitate the reader’s own
conclusions to a case study
4. Design a multiple-case case study that while covering multiple cases still draws a single set of
cross-case conclusions (single large organization, not multi-organizational). You will include
Lean Six Sigma specifically in the Design (type 4), Collect and Analysis (cross-case synthesis)
phases of your case study (use the Zhang et al. (2015) article as a model). [Also see Boxes 3, 32,
and 38 (Yin, 2018)]
Required Format
This 1600 minimum, 2400 maximum word paper needs to be written with these main sections:
Cover page
Abstract
Introduction
Case Study Report Audience and Reporting Methodology
Visual and Textual Materials of a Case Study Report
Reporting Evidence: Striking the Balance
Multiple-Case Case Study with Lean Six Sigma
Conclusion
References
Other Requirements
Materials submitted to fulfill requirements in one course may not be submitted in another course.
Concerns about the propriety of obtaining outside assistance and acknowledging sources should
be addressed to the instructor of the course before the work commences and as necessary as the
work proceeds.
The cover page must include this statement as an author’s note: “By submitting this
assignment, I attest this submission represents my own work, and not that of another
student, scholar, or internet source. I understand I am responsible for knowing and
correctly utilizing referencing and bibliographical guidelines. I have not submitted this
work for any other class.”

BUSI 830
In addition to the course textbook(s) and the Bible, this paper must include at least 5
references from scholarly articles that have publication dates no older than 5 years. Do
not use any books other than the Bible and the textbook. Do not conduct interviews.
There should be at least one instance of biblical integration (at least one scripture
reference).
In-text citations are required to support your statements, points, assertions, issues,
arguments, concerns, paragraph topic sentences, and statements of fact and opinion.
The required cover page, abstract and the reference pages are not included in the required
assignment word count but are required as part of your paper.
The APA required abstract and conclusion section headings and subject headings (see
above) are expected. For papers this length, there should be at least two (2) ‘levels of
headings’.
The introduction and conclusion sections should not be longer than ½ page each since the
assignment is short in word count.
The required abstract should be written as a stand-alone document and not written as an
introduction since an introduction section is required. Therefore, refrain from using
phrases such as, “in this paper,” and do not use citations. See example in APA manual.
Sources of information from Wikipedia, dictionaries, and encyclopedia will not be
accepted. Similarity scores must not exceed 20%.
Paragraph lengths: Each paragraph should have a topic sentence unless it continues from
or provides support to the prior paragraph. A paragraph is defined in this course as being
at least 4 sentences in length.
All parts of the assignment must be based on scholarly and biblical literature.
Avoid clichés, slang, jargon, exaggerations, abbreviations, figurative language, and
language that is too informal and too subjective.
Submit your final document for grading with file name syntax: Last NameFirst Initial
Project#. For example: PhilebaumJ Project6.doc (no .pdfs)
Grading Metrics
Consult the accompanying rubric for how your instructor will grade this assignment. Also, any
form of plagiarism, including cutting and pasting, will result in zero points for the entire
assignment. All quoted materials must be properly cited in current APA format.
Note: Your assignment will be checked for originality via the SafeAssign plagiarism tool.
BUSI 830
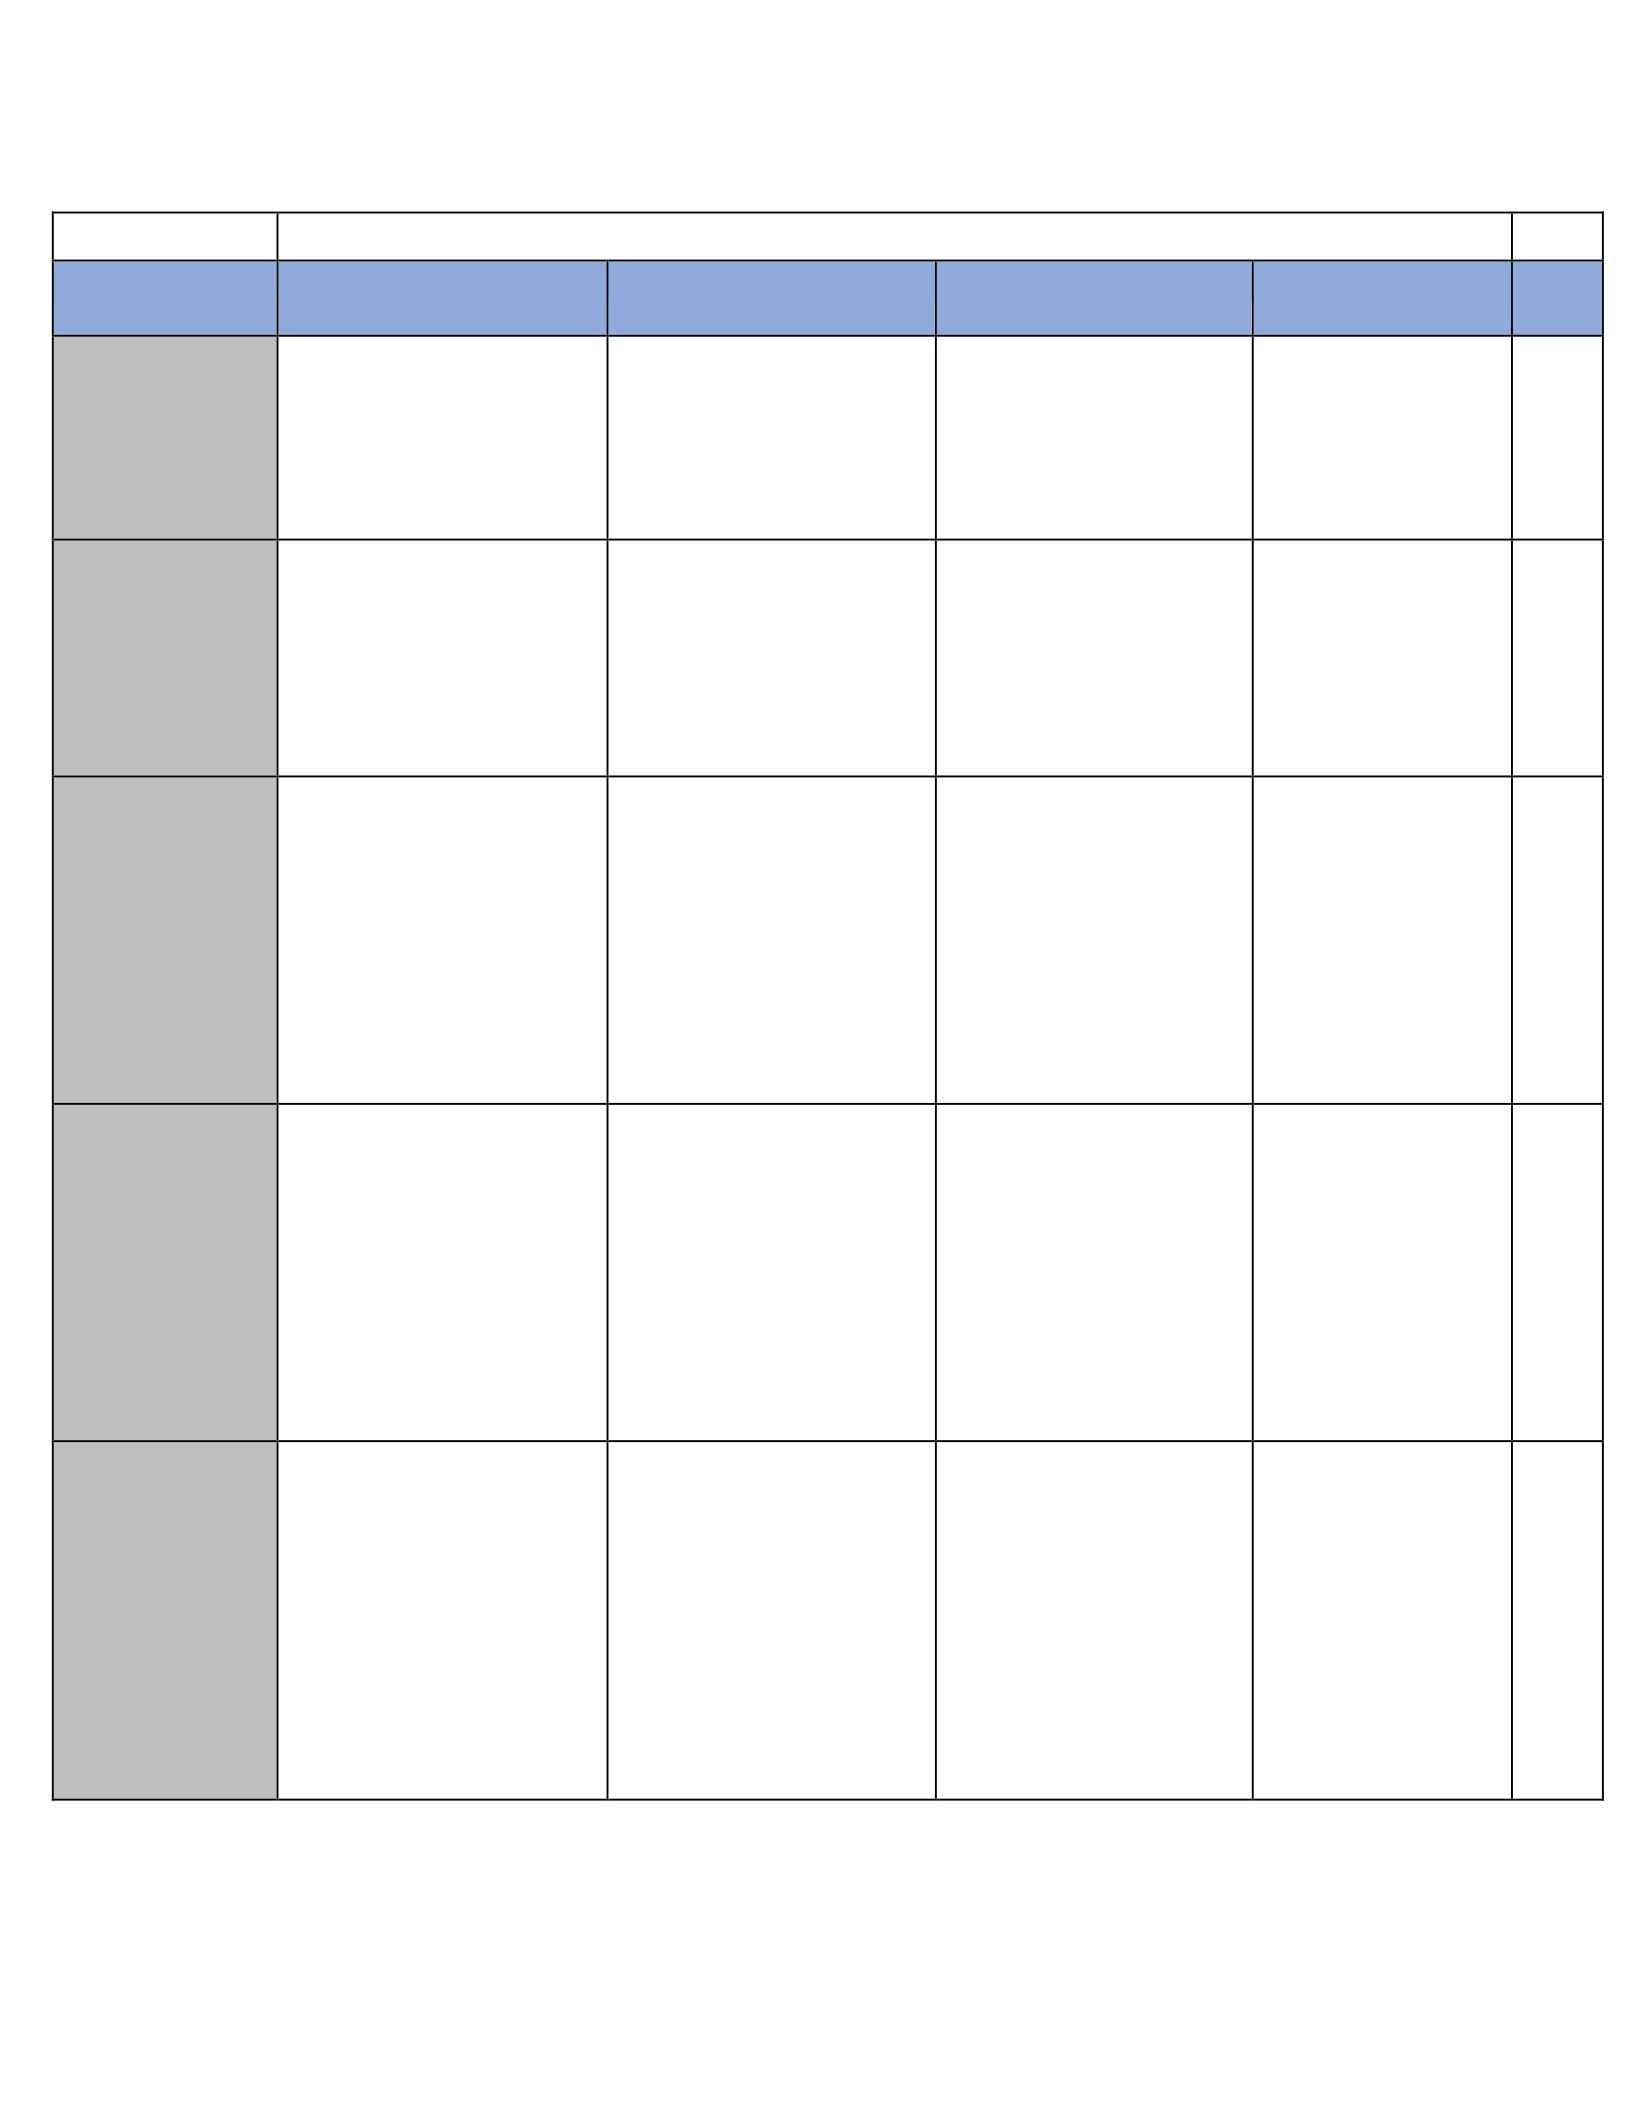
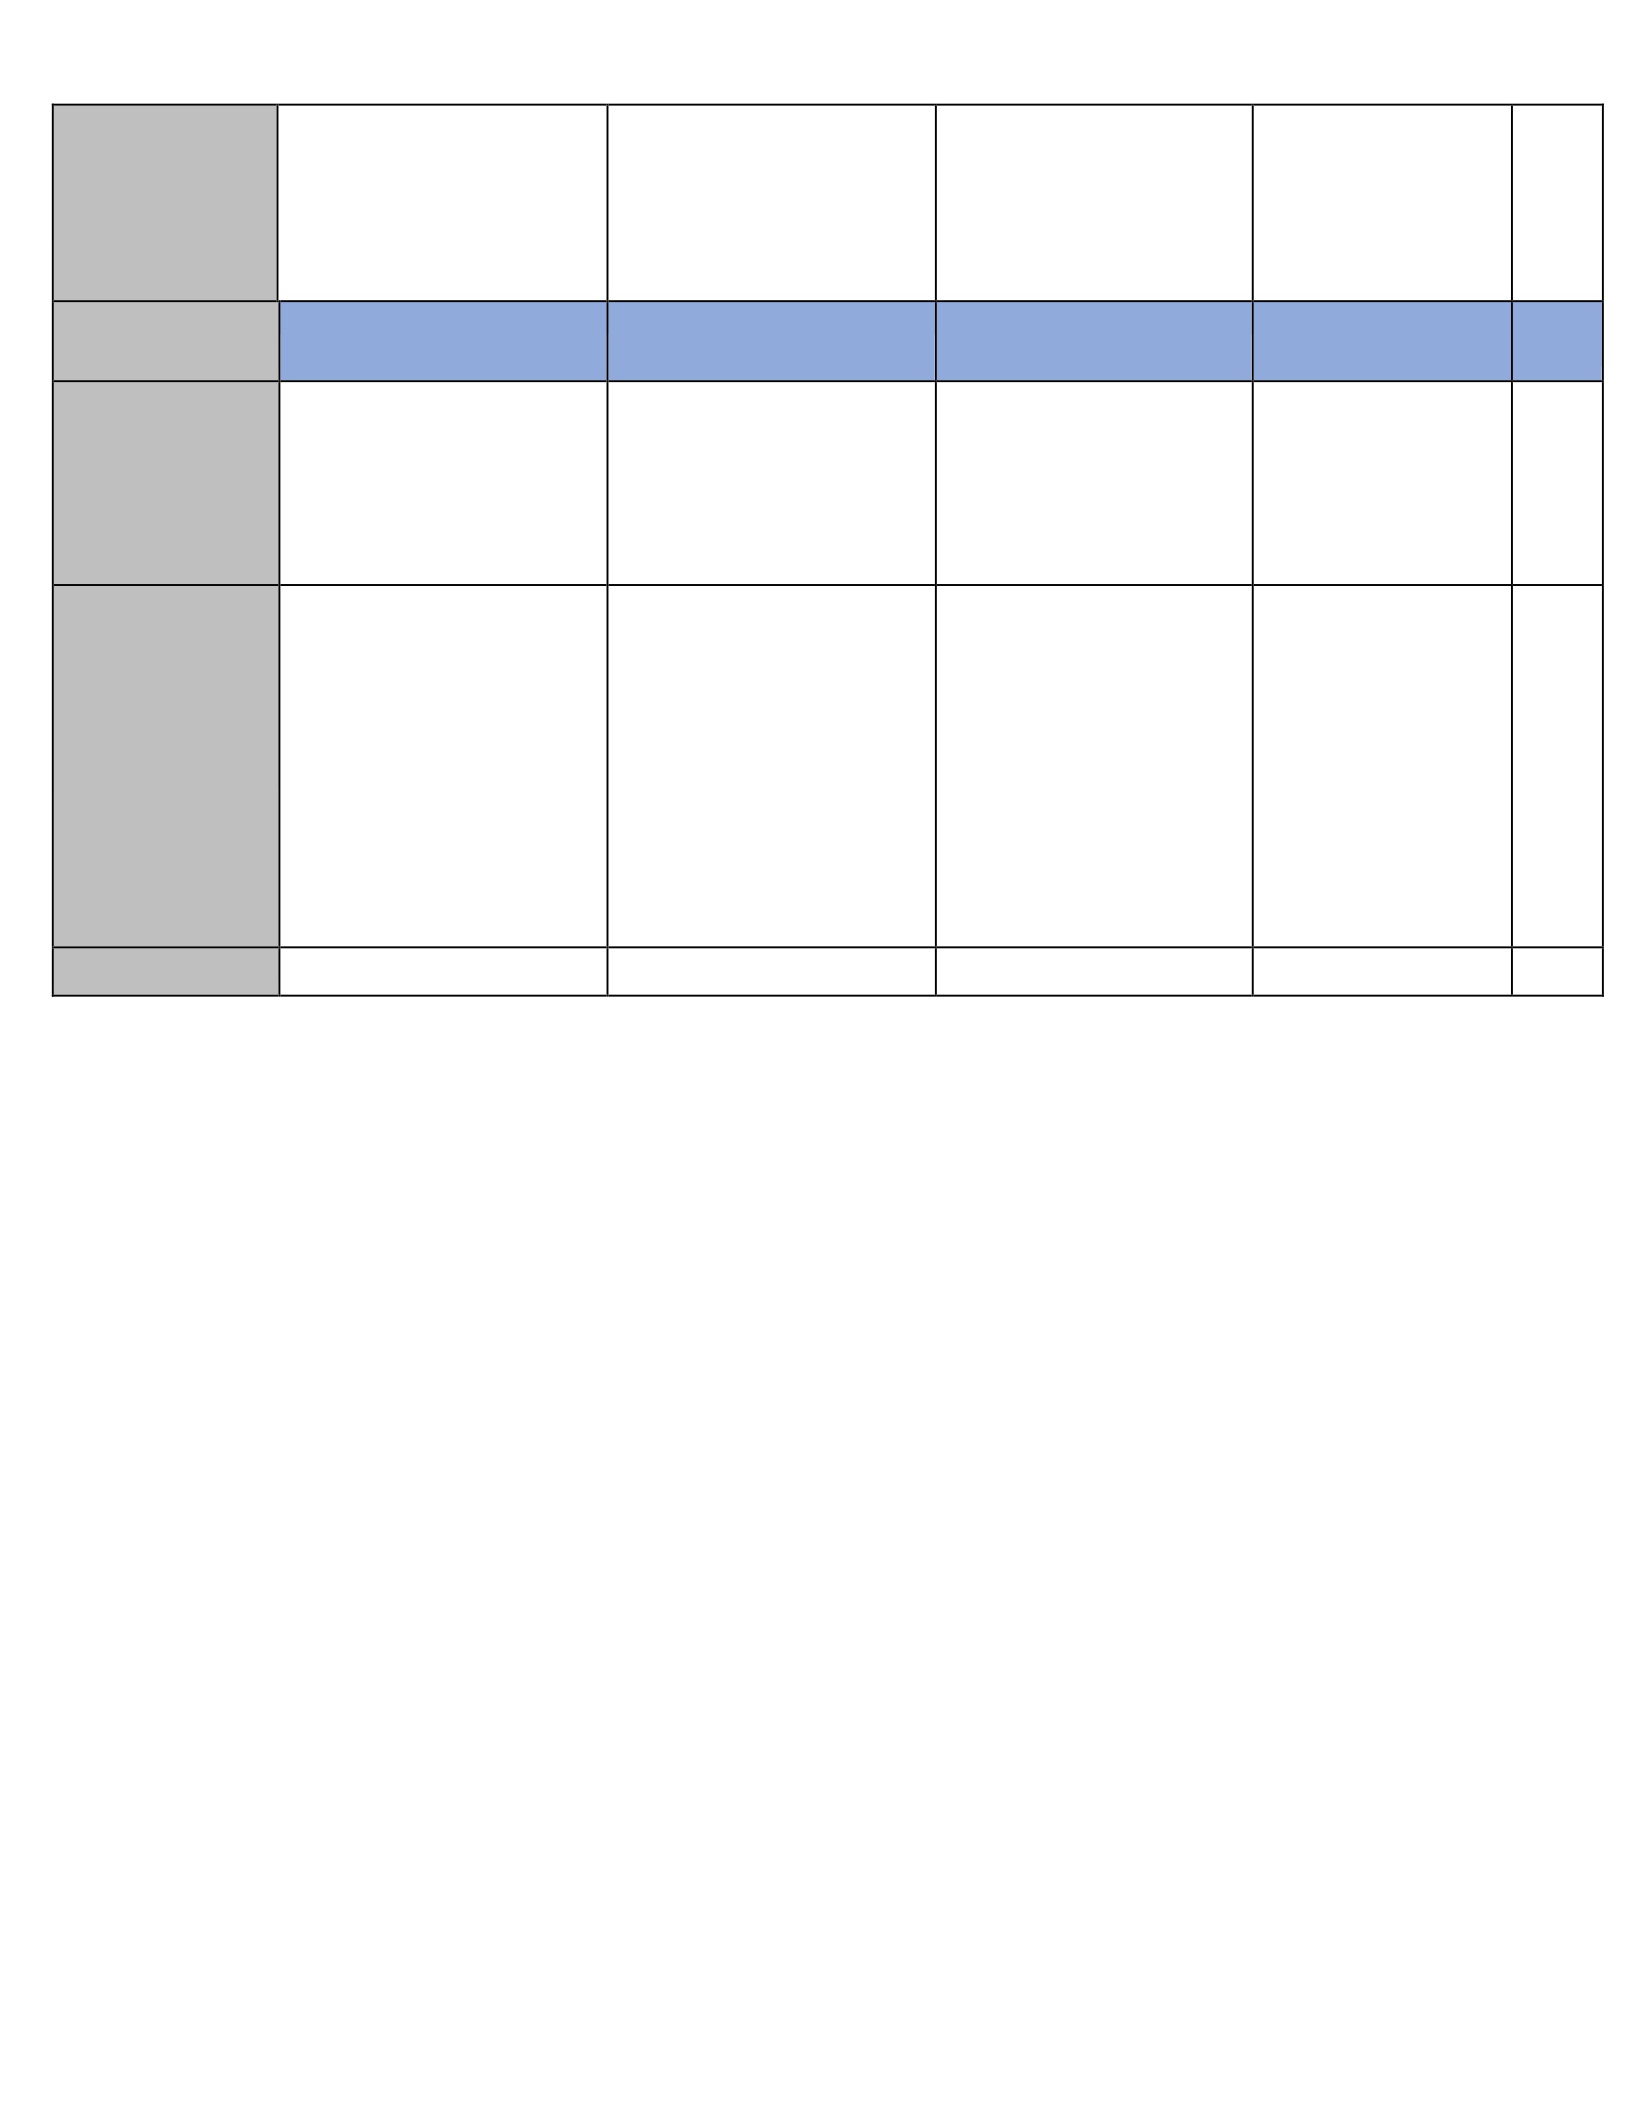
Multiple-Case Case Study Grading Rubric
Criteria
Levels of Achievement
Content ‐ 53 Points
Advanced
Proficient
Developing
Not present
Points
Earned
Abstract,
Introduction
5 Points
4 to 5 points
Abstract clearly states the
purpose and main conclusion
and Introduction provides a
complete overview of the
discussion.
2 to 3 points
Abstract and Introduction
provides a partial purpose,
main conclusion, and
overview of the discussion.
1 to 1 point
Abstract and Introduction
present but does not provide
an overview of the
discussion.
0 to 0 points
Not completed.
Case Study Report
Audience and
Reporting
Methodology
10 Points
9 to 10 points
Section provides a complete
discussion of the audience
and reporting methodology.
Flow is logical and fully cited.
6 to 8 points
Section provides a partially
complete discussion of the
audience and/or reporting
methodology. Flow is mostly
logical and partially cited.
1 to 5 points
Section provides a minimal
discussion of the audience
and/or reporting
methodology. Flow is not
logical and/or insufficiently
cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Visual and Textual
Materials of a Case
Study Report
10 Points
9 to 10 points
Section provides a
comprehensive description of
visual and textual materials of
a Case Study Report. Flow is
logical and fully cited.
6 to 8 points
Section provides a partial
description of visual and
textual materials of a Case
Study Report. Flow is logical
and partially cited.
1 to 5 points
Section provides a minimal
description of visual and
textual materials of a Case
Study Report. Flow is not
logical and/or insufficiently
cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Reporting
Evidence: Striking
the Balance
10 Points
9 to 10 points
Section provides a complete
and thorough discussion of the
appropriate balance of
evidence to provide to be
comprehensive and yet
enough for the reader to draw
their own conclusions to the
case study. Flow is
logical and fully cited.
6 to 8 points
Section provides a partial
discussion of the appropriate
balance of evidence to
provide to be comprehensive
and yet enough for the reader
to draw their own conclusions
to the case study. Flow is
mostly logical and partially
cited.
1 to 5 points
Section provides a minimal
discussion of the appropriate
balance of evidence to
provide to be comprehensive
and yet enough for the
reader to draw their own
conclusions to the case
study. Flow is not logical
and/or insufficiently cited.
0 to 0 points
Not completed or not
related to requirements
for the section.
Multiple-Case Case
Study with Lean
Six Sigma
10 Points
9 to 10 points
Demonstrates critical thinking
to include analysis, evaluation,
and synthesis of the course
material to draft a multiple-
case case study integrated
with Lean Six Sigma in the
Design, Collect and Analyze
phases.
6 to 8 points
Mostly synthesized the course
material to draft a multiple-
case case study integrated
with or without Lean Six
Sigma in the Design, Collect
and/or Analyze phases.
1 to 5 points
Only partially demonstrated
critical thinking, analysis,
evaluation, and/or limited
synthesis of the course
material to draft a multiple-
case case study integrated
with or without Lean Six
Sigma in the Design, Collect
and/or Analyze phases.
0 to 0 points
Not completed or not
related to requirements
for the section.
BUSI 830
Conclusion &
Biblical Integration
8 Points
8 to 8 points
Conclusion provides a
complete summary of the
discussion and highlights key
points and robust biblical
integration is present.
7 to 7 points
Conclusion provides a partial
summary of the discussion
and highlights at least one key
point and some biblical
integration is present.
1 to 6 points
Conclusion present but does
not summarize discussion or
highlight key points and little
to no biblical integration is
present.
0 to 0 points
Not completed.
Structure ‐ 22
Points
Advanced
Proficient
Developing
Not present
Points
Earned
Mechanics,
Composition,
Grammar, Word
Count
11 Points
11 to 11 points
Mechanics, Composition, &
Word Count is thorough
(1600-2400 words).
10 to 10 points
Mechanics, Composition, &
Word Count is satisfactory (+/-
2%).
1 to 9 points
Mechanics, Composition, &
Word Count is insufficient
(+/- 3-4%).
0 to 0 points
There are many errors
in mechanics,
composition, grammar
or Word Count (>4%
diff).
APA Format,
Structure, &
References and
Citations
11 Points
11 to 11 points
Proper cover page and
section headings included.
Met all of the required
formatting. References
exceed requirements in
number and quality and/or
most statements are
supported by a variety of
citations.
10 to 10 points
Proper cover page and
section headings included.
Met most of the required
formatting. References meet
requirements in number and
quality and/or many
statements are supported by a
variety of citations.
1 to 9 points
No cover page and/or section
headings included. Met some
required formatting.
References do not meet
requirements in number and
quality and/or some
statements are supported by
a variety of citations.
0 to 0 points
No structure or
formatting provided.
Missing references
and/or citations are
rare, repetitious or non-
existent.
Total Points
/75
Instructor’s Comments:
Full Terms & Conditions of access and use can be found at
https://www.tandfonline.com/action/journalInformation?journalCode=tppc20
Production Planning & Control
The Management of Operations
ISSN: 0953-7287 (Print) 1366-5871 (Online) Journal homepage: https://www.tandfonline.com/loi/tppc20
Comprehensive Six Sigma application: a case study
Min Zhang, Wei Wang, Thong Ngee Goh & Zhen He
To cite this article: Min Zhang, Wei Wang, Thong Ngee Goh & Zhen He (2015) Comprehensive
Six Sigma application: a case study, Production Planning & Control, 26:3, 219-234, DOI:
10.1080/09537287.2014.891058
To link to this article: https://doi.org/10.1080/09537287.2014.891058
Published online: 10 Mar 2014.
Submit your article to this journal
Article views: 1784
View related articles
View Crossmark data
Citing articles: 7 View citing articles
Comprehensive Six Sigma application: a case study
Min Zhang
a
*, Wei Wang
a
, Thong Ngee Goh
b
and Zhen He
a
a
College of Management and Economics, Tianjin University, No. 92, Weijin Road, Nankai District, Tianjin, China;
b
Department of
Industrial and Systems Engineering, National University of Singapore, Singapore, Singapore
(Received 20 March 2013; accepted 29 January 2014)
Six Sigma as a framework for eliminating defects at the project level and improving performance and customer satisfaction
at the corporate level has been generally recognised. This case-oriented paper reports an important Six Sigma management
case study at the world’s largest cold rolling mill situated in China. The descriptions of measures taken at the company
level, as well as that of the exemplary application experience of this company, would constitute a most comprehensive
account of the impact brought about by Six Sigma to the company. A Black Belt project was conducted to improve the cold
rolling capability to meet the thickness requirements using the Six Sigma methodology –DMAIC (define, measure, analyse,
improve and control) principle. The implementation of Six Sigma methodology led to a significant financial impact on the
profitability of the company. Seven key factors were also found to be instrumental to the successful Six Sigma management
implementation in the company.
Keywords: Six Sigma; DMAIC; quality management; quality improvement; metallurgy; China
1. Introduction
Six Sigma is a systematic methodology aimed at operational
excellence through continuous process improvements. As we
know, although Six Sigma originated from Motorola in 1986
arising from the need to improve product quality and cus-
tomer satisfaction in the face of fierce competition from
Japan, some of the basic approaches and tools of Six Sigma
originated from the widespread application of statistical
methods in the American military industry since the Second
World War (Deming 1993). The procedures to obtain varia-
tion reduction systematically by statistical means or methods
were given by Shewhart and Deming. The essential nature
of ‘Six Sigma’is ‘confidence building’, which in turn makes
it easier for a company to direct (modify, maintain and pre-
vent) the behaviour of ‘people’(customers, vendors, employ-
ees, etc.) in a manner that sustains the survival or growth of
the company (Christiansen 2011).
It is noteworthy that Aboelmaged (2010) pointed out that
case study is the most dominant research method in Six
Sigma articles (55.4% in 231 articles). There have been
reports on gains in financial benefits and competitive
advantages arising from Six Sigma applications from various
countries and districts (e.g. Bañuelas, Antony, and Brace
2005; Desai 2006; Kumar et al. 2006; Anand et al. 2007;Su
and Chou 2008; Aksoy and Orbak 2009; Chakravorty 2009;
Chen and Lyu 2009; El Haouzi, Petin, and Thomas 2009;
Lo, Tsai, and Hsieh 2009;YangandHsieh2009;Chenetal.
2010;Jouetal.2010; Zu, Robbins, and Fredendall 2010;
Gijo, Scaria, and Antony 2011;Lietal.2011; Antony, Gijo,
and Childe 2012; Bilgen and Sen 2012; Tanik and Sen 2012;
Ghosh and Maiti 2012;Linetal.2013). Although Six Sigma
wasintroducedtoChinasoonafteritsinceptioninAmerica
in the 1980s and an increasing number of Chinese compa-
nies are implementing or planningtodeploySixSigma,
research and case studies of Six Sigma implementation in
Chinese companies have seldom been reported until now. In
this paper, we present a case of comprehensive Six Sigma
application in a large stainless steel company, through the
illustration of an overall Six Sigma implementation strategy
and a successful project, to furnish an insight into the poten-
tial impact of Six Sigma in the industrial sector of the
world’
s second largest economy.
The paper is organised as follows. Section 2presents
the overall Six Sigma implementation strategy of Com-
pany T. Section 3illustrates how DMAIC (define, mea-
sure, analyse, improve and control) is used to solve an
important problem in what is referred to as Company T.
Section 4presents the economic benefits of this Black Belt
project. Section 5consists of a discussion of the key fac-
tors of successful Six Sigma management implementation;
the last section presents the major conclusion of the paper.
2. Company-level Six Sigma implementation at
‘Company T’
2.1. Six Sigma start-up
The case study is related to quality management in a
stainless steel cold rolling mill, which for the purpose of
© 2014 Taylor & Francis
Production Planning & Control, 2015
Vol. 26, No. 3, 219–234, http://dx.doi.org/10.1080/09537287.2014.891058

this presentation is referred to as ‘Company T’. The
company’s Six Sigma promotion approach is first intro-
duced, and then a Black Belt project related to the thick-
ness of stainless steel cold rolling sheet is described
along with the economic benefits.
Company T, founded in 1934, is a ‘mega’enterprise
in iron and steel encompassing iron mining, production,
machining, distribution and trading. It is also the largest
stainless steel enterprise in the world with advanced
technologies and equipments, complete product types
and specifications. Its annual production capability is
about 10 million tons of steel, including 3 million tons
of stainless steel.
As a conventional state-owned enterprise, Company
T has been in constant search for effective quality man-
agement methods. For example, quality control circles
have a history of more than two decades; in early 1990s,
the company began to implement ISO9000 and was cer-
tified. These efforts have played an important role in
motivating the staff and solving on-site quality problems.
With the rapid development of the company and the
need for continuous improvement in quality, statistical
process control theory and methods have been deployed
to enhance quality performance. Various quality manage-
ment techniques, such as 5S, TPM and JIT, have been
implemented as well, in efforts to improve site manage-
ment, elevate operational efficiency of equipment and
facilitate on-time production.
At the turn of the century, it was determined that to
build a globally competitive stainless steel enterprise, it
takes a breakthrough from management by experience to
management by scientific tools. Thus, QC circles were
found to be inadequate in handling inter-process, inter-
departmental quality issues, while teams with responsibili-
ties in quality improvement would face a lack of system-
atic improvement procedures and effective analytical
tools. And the deployments of QC circles, TPM, 5S and
other initiatives belong to different departments, and col-
laborations among them were less common. Thus, the
potential of these initiatives is not fully utilised. The
reported successful experience of domestic as foreign
companies such as Posco of Korea led to the strategic
decision, in 2004, by the leadership of Company T to turn
to Six Sigma management, which made the company one
of the earliest among steel enterprises in China to embrace
Six Sigma.
With high-level management commitment, the com-
pany drew up the 2006–2010 Five-Year Plan for Six
Sigma management. The entire company senior manage-
ment team attended the introductory training. And with
the five-year plan, the company chairman took the lead for
its implementation, set up a company Six Sigma office,
with additional rewards to those promoting Six Sigma.
The company CEO initiated the corresponding human
resource incentives, attended meetings for Six Sigma
promotion and project selection, and secured various
needed resources. As Six Sigma champion, the chief engi-
neer took the lead for formulating annual Six Sigma pro-
motion plans, identifying improvement projects,
conducting project reviews and promoting the presence of
a Six Sigma culture in general.
2.2. Integration of Six Sigma and other initiatives
Like many other Chinese state-owned enterprises, Com-
pany T faced some problems raised by some employees.
Typical questions were: What are the differences between
Six Sigma and other management initiatives? and How
can we balance the resources required by Six Sigma and
other methods such as TQM, Lean Production and TPM?
With the help from outside consultants, Company T rea-
lised that the core values of Six Sigma and other manage-
ment initiatives are basically the same. The advantages of
Six Sigma are: (1) Six Sigma provides a systematic infra-
structure and mechanism for continuous improvement
through strong top-down management commitment; (2)
Though Six Sigma does not bring about any new tools,
and actually Six Sigma tools and methods existed before
the name Six Sigma was coined, Six Sigma provides a
clear and easy-to-implement DMAIC roadmap for busi-
ness process improvement, with DMADV (Define, Mea-
sure, Analyse, Design and Verify) or IDDOV (Identify,
Define, Develop, Optimise and Verify) and other roadmap
of design for Six Sigma for product/process design and
innovation; (3) The effective project management and rig-
orous problems-solving tools of Six Sigma provides a
general framework for problem identification, problem
analysis and problem-solving. Thus, Six Sigma project
can reach accountable business results; and (4) The sys-
tematic action-learning-type training of Black Belts, Green
Belts and Yellow Belts provides an effective and efficient
talent cultivation system. Thus, Six Sigma can be inte-
grated with Lean Production, TPM and other management
initiatives. And there are many successful stories of Six
Sigma integration. Thus Company T builds a big Six
Sigma umbrella at corporate level, which includes QCC
(Company T puts it as Quick Six Sigma projects), TPM
and Lean Production, etc.
2.3. Organisation for implementation
The Six Sigma management style in Company T focuses on
the full participation of all employees, with fast and continuous
improvements. The strategy and main thrusts are as follows.
2.3.1. Full participation
All employees are required to learn the basic principles
and contents of Six Sigma management through various
familiarisation programs and training. Every employee is
220 M. Zhang et al.

expected to be able to make good use of Six Sigma
ideas appropriate to their work responsibilities.
2.3.2. Multi-level and systematic organisation structure
The first level encompasses quality-related teams or pro-
jects, related to complete processes, systems and long-
term activities; members comprise all related staff and
the main management and technical personnel.
The second level comprises ‘contract’project teams
aiming at solving specific quality problems and optimisa-
tion of management processes; team members consist of
technical and management specialists and experts.
The third level are ‘Quick Six Sigma’(QSS) teams
with projects focusing on existing problems and quick
improvements: depending on the depth and breadth of
the study, projects are categorised into those for Black
Belts (BB), Green Belts (GB) and Yellow Belts; team
members are made up of engineers, managers and opera-
tors directly related to the specific processes in question.
The fourth level is based on Lean Six Sigma pro-
jects, addressing work standardisation as well as opera-
tions quantification and control; the bulk of the team
members are related operators.
2.3.3. Quick and continuous improvement
The multi-level structure of Six Sigma implementation
teams is formed to solve business problems of strategic
level and operational level. And this structure helps
Company T form the critical mass of Six Sigma. Thus,
Company T builds up a continuous improvement model
based on Six Sigma. On one hand, the ready formation
of different level Six Sigma teams to address critical
business issues as well as operational situations ensures
timely concentration of resources for problem-solving.
On the other hand, it is recognised that there is no finish-
ing line for quality improvement; thus, persistent Six
Sigma improvement efforts are essential: as soon as the
targets of one stage are reached, new ones are set for
further gains in quality performance.
3. Black Belt project: sheet thickness improvement
A significant Black Belt project in the context of the above
company-wide Six Sigma improvement effort will now be
presented. The project is about improving the capability to meet
the thickness requirements of stainless steel cold rolling sheets.
3.1. Background of project
Stainless steel cold rolling sheet is the most competitive
product in Company T. The thickness of the cold rolling
sheet is recognised as the key quality characteristic.
Thickness variation control not only reflects product
quality, but also has a close relationship with the eco-
nomic benefits that can be derived by the customers.
However, from market surveys and customers’responses,
the thickness variation of cold rolling sheet produced in
Company T has been too large. Through benchmarking
with its competitor Company P, Company T found that
the means of its cold rolling sheet thickness are about
0.01–0.04 mm larger than the corresponding values in
Company P, and the variation is quite larger than its
competitor’s. Thus, the managers in the cold rolling mill
made the decision to have a Six Sigma project aimed at
decreasing the variation of thickness and improving the
thickness compliance of stainless steel cold-rolled sheets
to enhance the market competitiveness of their products.
The team members were trained to use Minitab software
to do statistical analysis. In this paper, all statistical anal-
ysis outputs are based on Minitab.
3.2. Definitions
3.2.1. Definition of non-conforming product
Based on quality inspection standards, the thickness of
steel rolls is measured as the vertical diameter of steel
sheet. If the thickness of a roll is within the upper and
lower specifications, then the roll is regarded as a con-
forming product, otherwise it is non-conforming.
3.2.2. Definition of yield
Total inspection is used here. The number of wholly
tested rolls is the denominator and the number of con-
forming rolls is the numerator. Thus, this ratio is taken
as the yield of the production line.
3.2.3. Goal of the Black Belt project
The thickness yield in Company T is only 68.9% now.
However, it is 85.2% in Company P. Through team work
analysis using SMART (specific, measurable, attainable,
relevant and time-bound) rule, the goal of this Black Belt
project is to increase the yield in Company T to 90%.
3.2.4. Team members
The chief engineer in Company T acts as the project
champion. Through Supplier, Input, Process, Output,
Customer and project stakeholder analysis, we found that
several departments are involved in this project including
the technical department (product and process design),
testing, equipment maintenance, etc. A cross-functional
team is formed including team members from each
department. Also, some experienced front line workers
are invited to be extended team members. A Black Belt
from technical department works as the team leader. The
Production Planning & Control 221
team makes a detailed project plan and reaches consen-
sus on the conduct of behaviour for the project activities.
3.3. Measure
3.3.1. Measurement system analysis
The cold rolling sheet thickness leads to continuous data.
The measurement system is analysed based on the thick-
ness data measured by micrometre and four testers. The
measurement system analysis is shown in Table 1. It can
be seen that the variance of total gauge R&R% is only
1.49% of the total variance, and the number of distinct
categories is 94. Thus, the capability of this measurement
system is reliable.
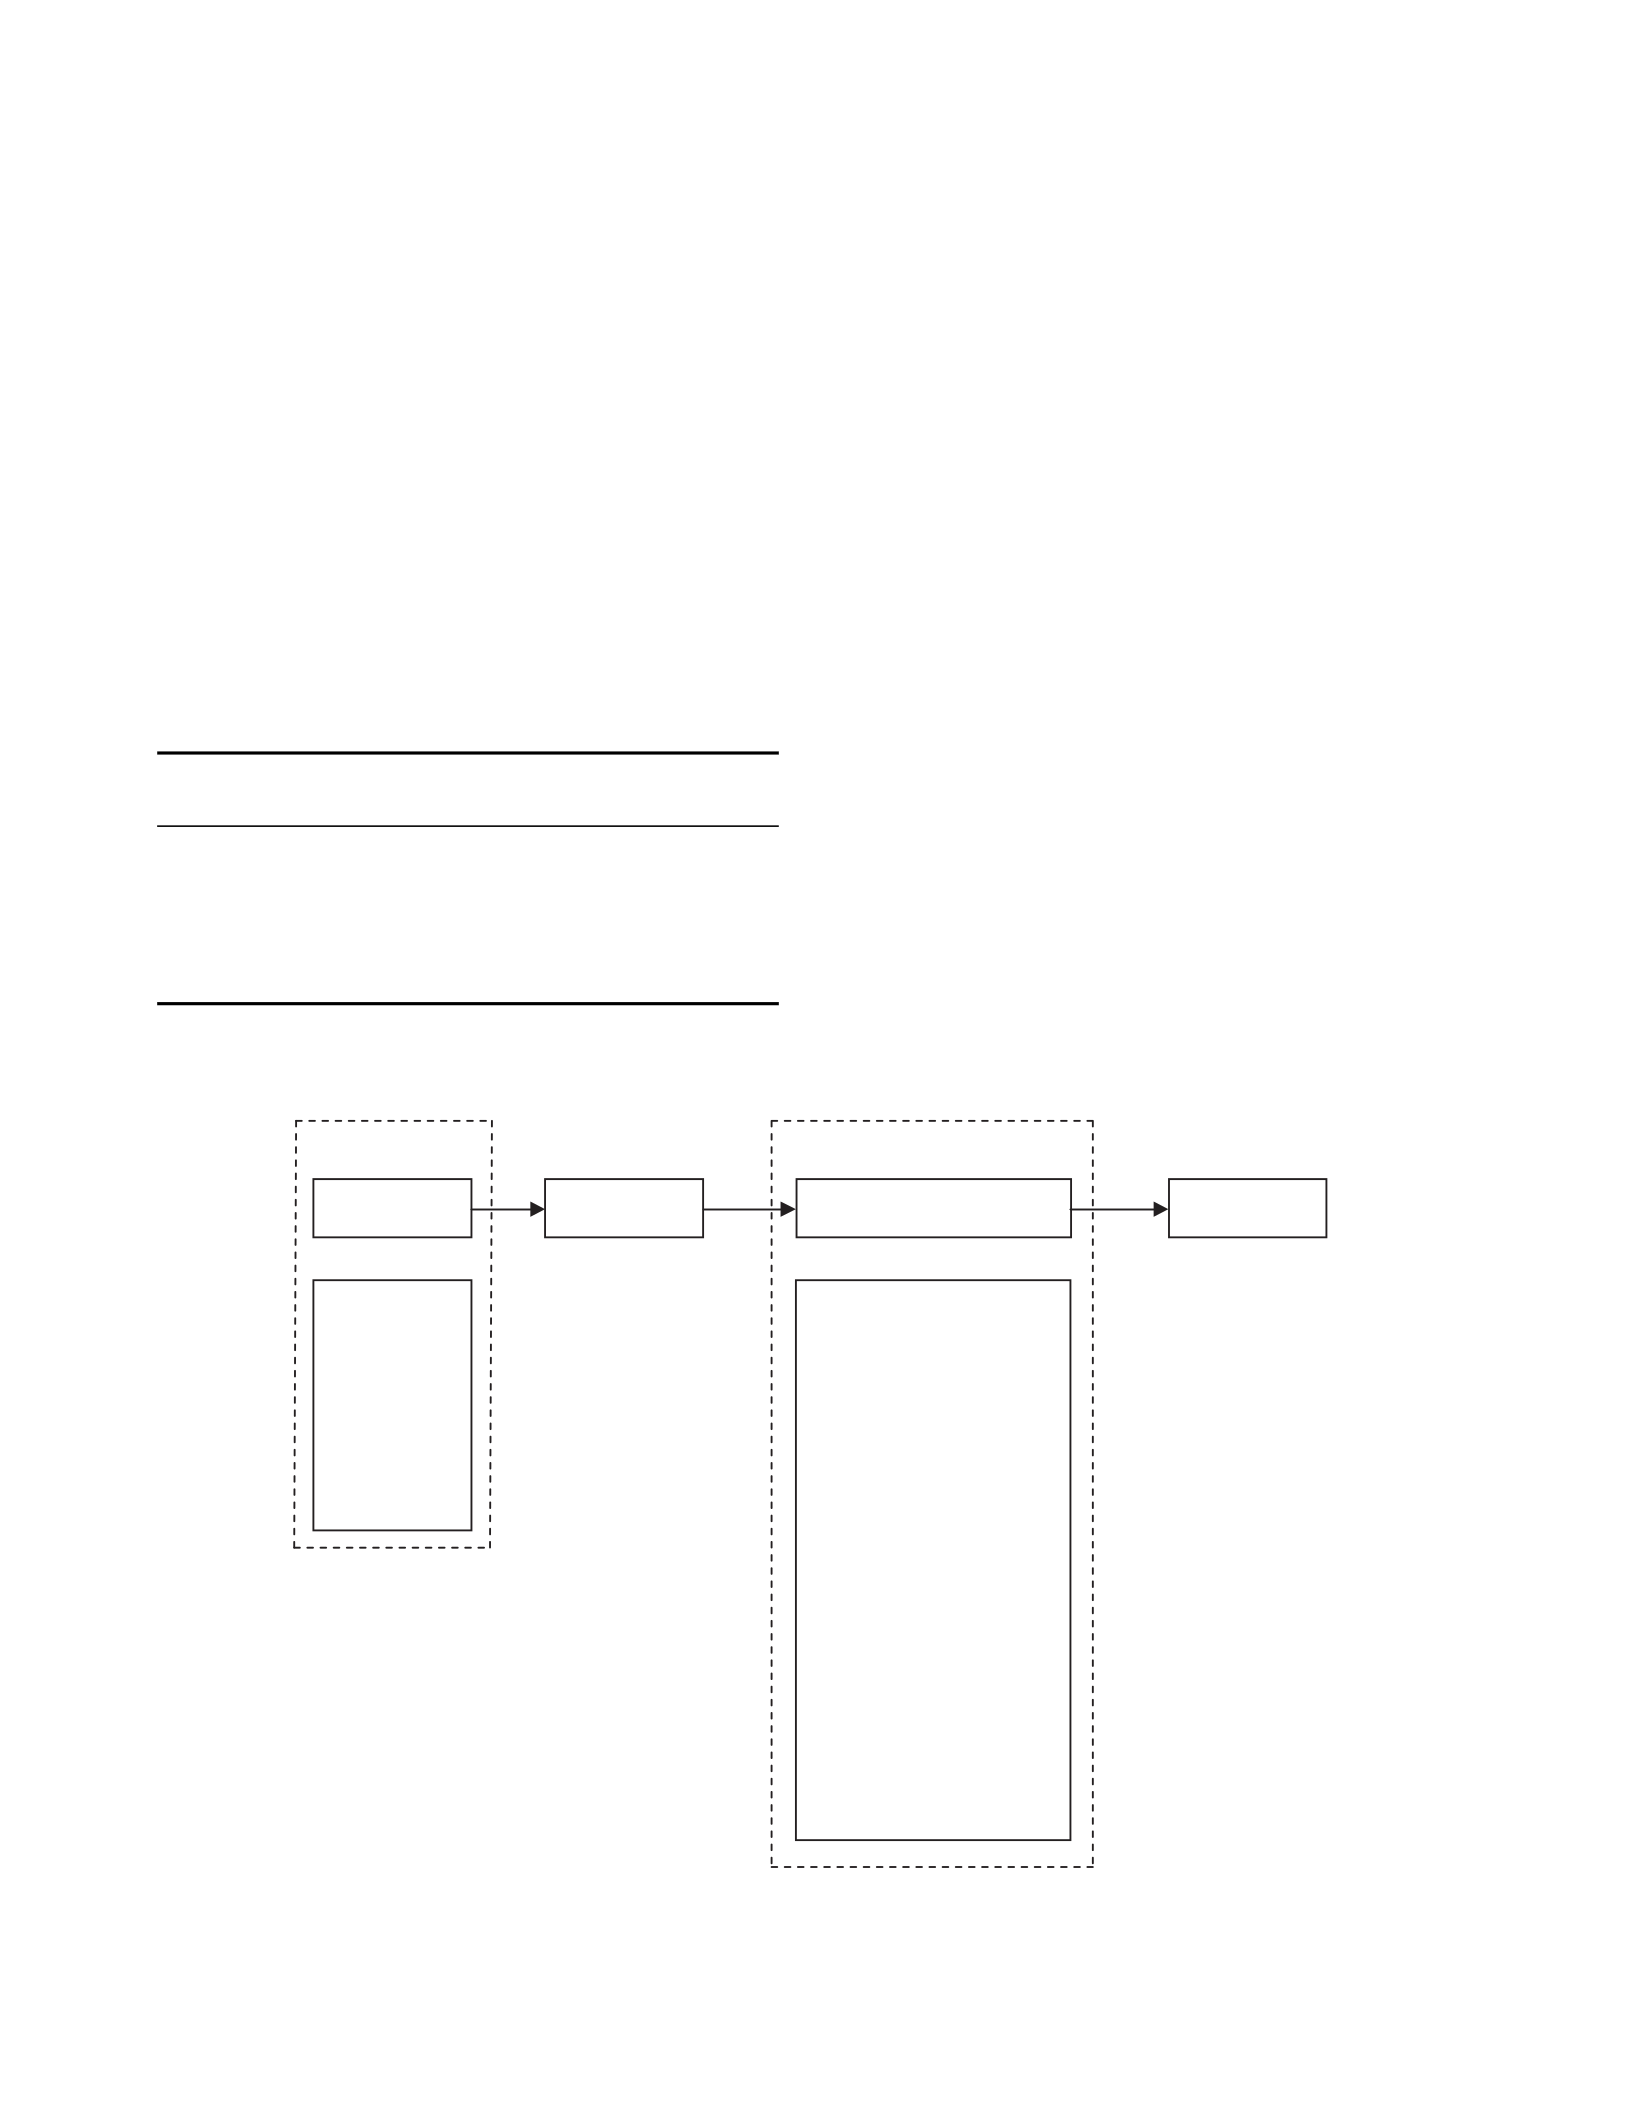
3.3.2. Process flow analysis and key process input
variables identification
In cold rolling mill, the key process is the rolling pro-
cess, for which the flow chart is shown in Figure 1. For
each process step in rolling, we identified the possible
factors that may impact the thickness of the stainless
steel plate. The cause and effect diagram as shown in
Figure 2is then used to find the main factors that might
influence the large sheet thickness variation from consid-
erations of human, machine, materials and method ele-
ments, aided by the brainstorming process. Eventually
32 potential factors are identified.
3.4. Analyse
3.4.1. Factors selected
In this project, the defect is thickness of out specification
including large thickness variation and extra thickness.
Here, a cause-and-effect matrix is used to show the rela-
tionship of these 32 factors and the defects. The impor-
tance of defects is set up by its weighted score in
Table 2. Nineteen factors (bold type in Table 2) with
total score larger than 50 are selected as key factors
related to the main defects. Next, a failure mode and
effect analysis (FMEA) is carried out for these factors,
as shown in Table 3.
Table 1. Measurement system analysis of stainless steel cold
rolling sheet thickness.
Source
Study var. % study Var.
Std. dev. (SD) (6 × SD) (% SV)
Total gauge R&R 0.010973 0.06584 1.49
Repeatability 0.010452 0.06271 1.42
Reproducibility 0.003340 0.02004 0.45
Operator 0.003340 0.02004 0.45
Part-to-part 0.737699 4.42620 99.99
Total variation 0.737781 4.42669 100.00
Note: Number of distinct categories = 94.
Input
variables:
Coils of hot
plate after
annealed and
pickling
Uncoiling Stretching Rolling Coiling
Input variables:
Thickness set
Roller type
Power source
Rolling pressure
Pull type
Standard plates
Rolling deformation rate
Type of steel
Rolling oil
Rolling pass
Defects:
Thickness of out
specification
Figure 1. The flow chart of cold rolling process.
222 M. Zhang et al.
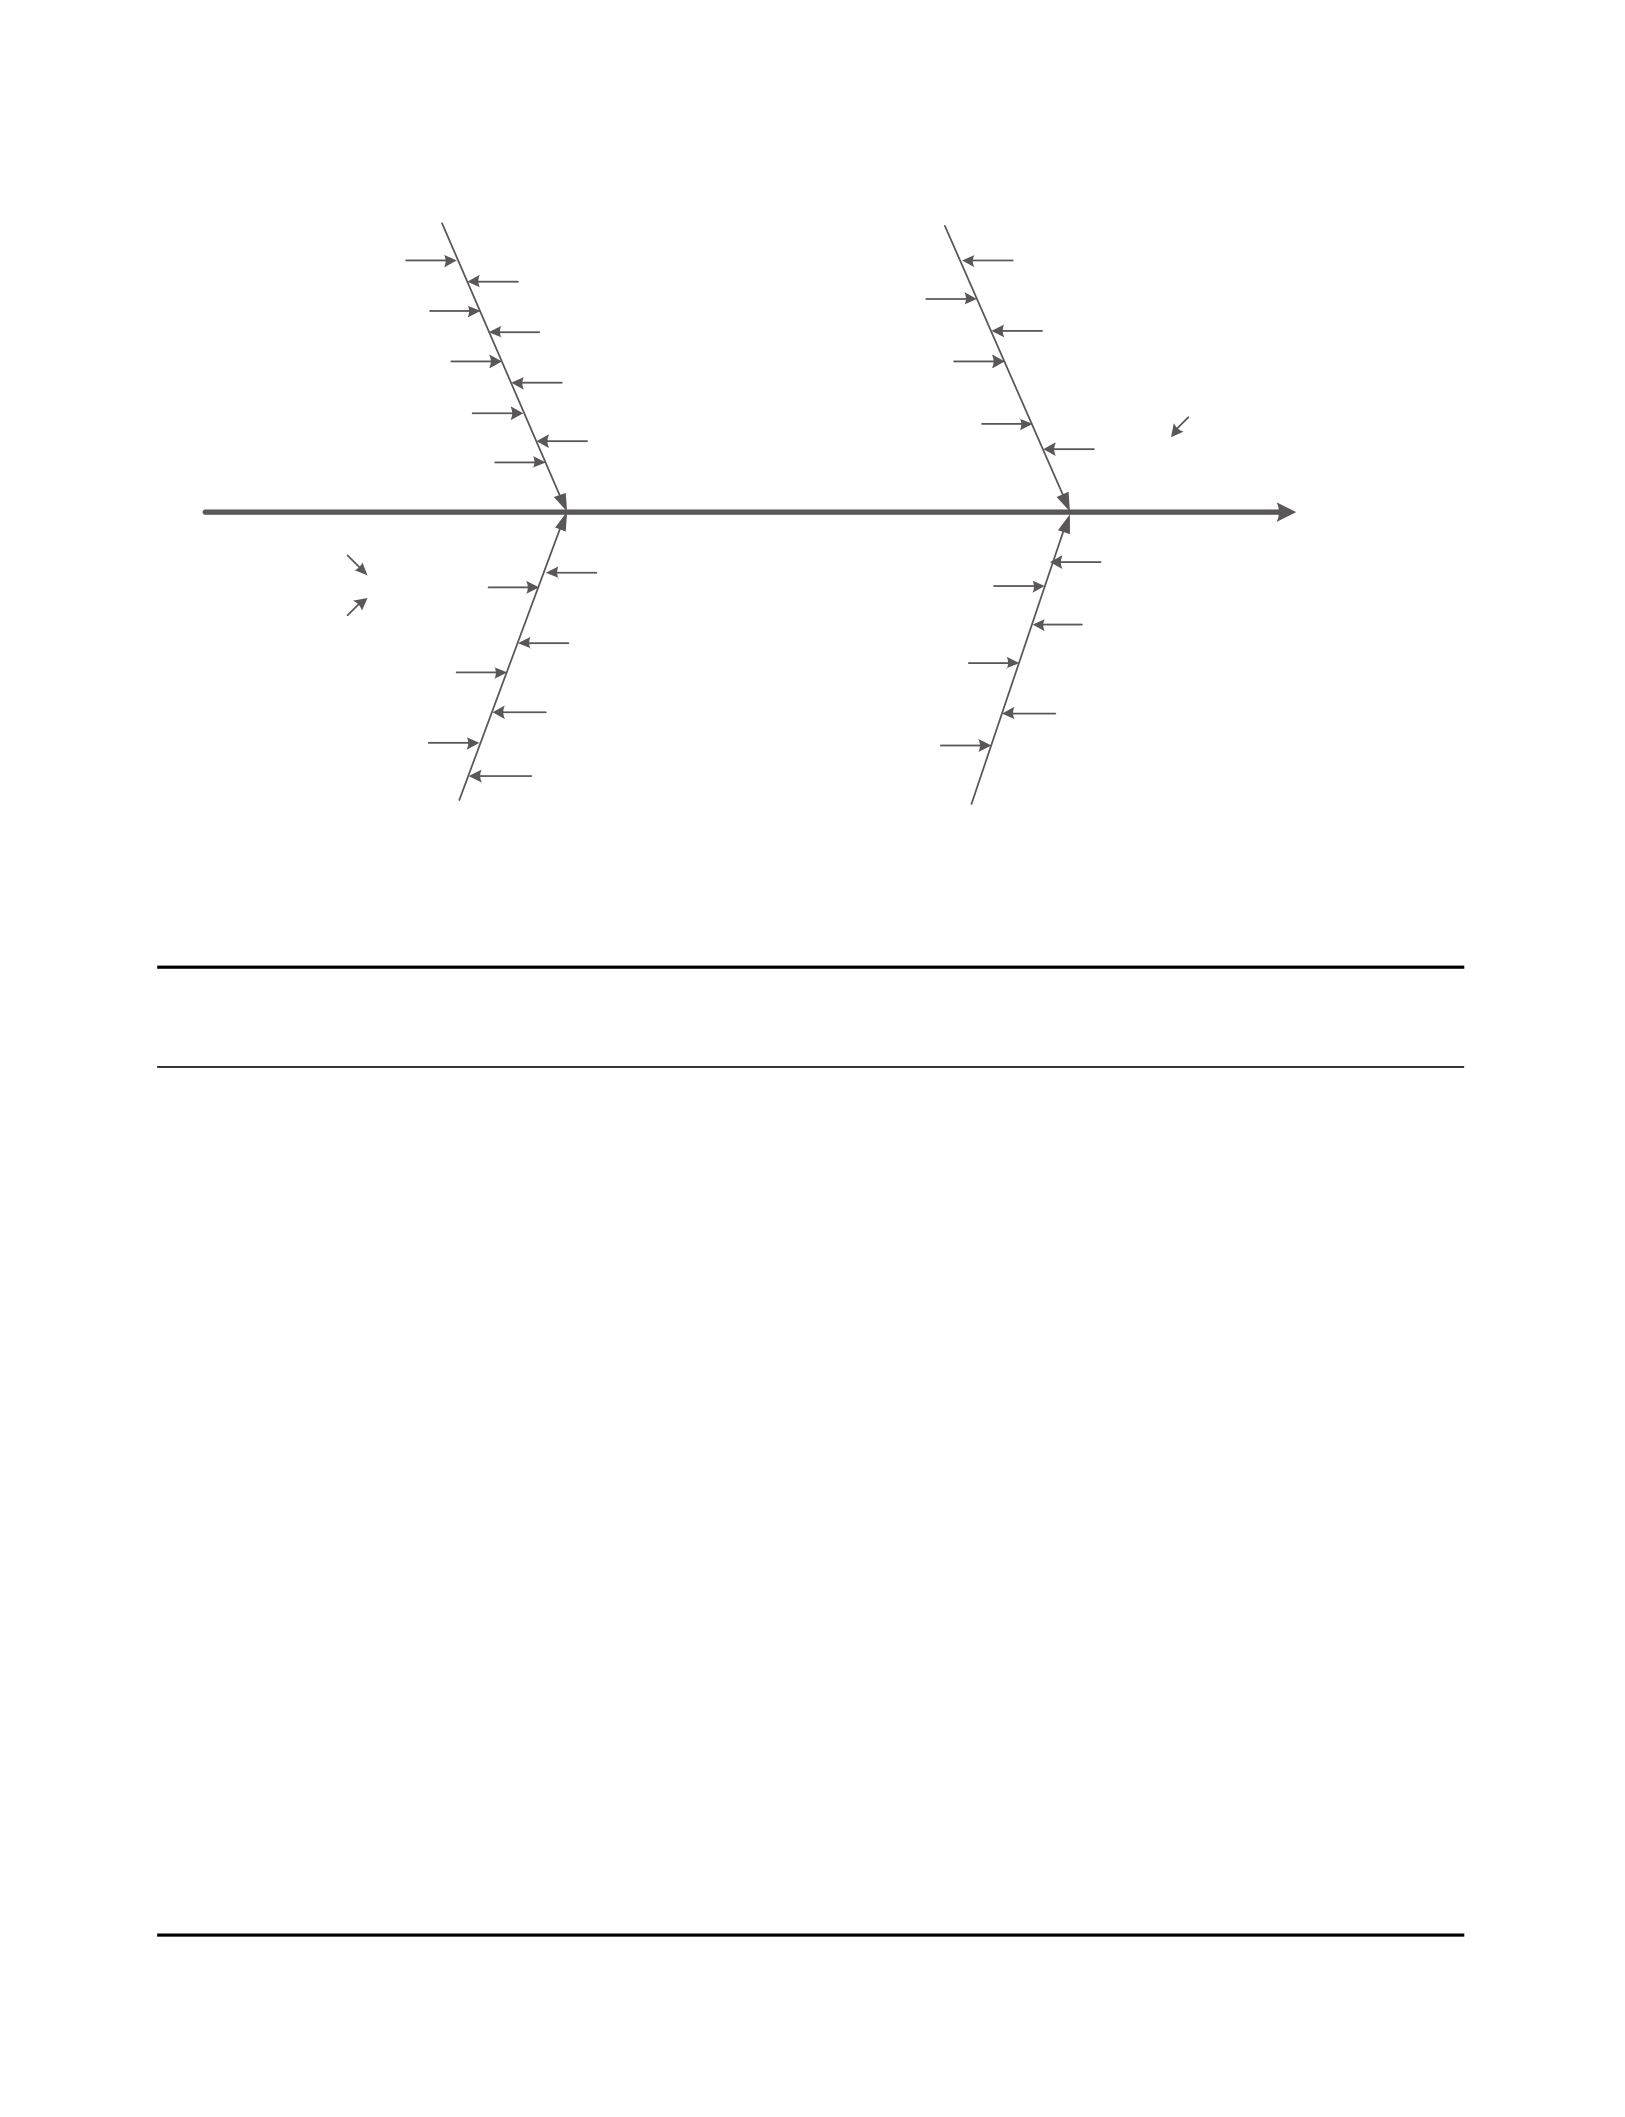
Effect of plate
temperature
Oil of steel plates
Foreign matter in
radioactive source
Unreasonable
compensating factor
Effect of heavy metal
elements in steel rolls
Abnormal failure
Effect of rolling oil
Uncorrected thickness
of standard plates
Uninitialized
Thickness Gauge
Not executing
set values
False use
of micrometer
Wrong input
of steel type
Wrong measurement
No training or poor training
Not measuring
thickness manually
Not checking
ERP information
Operator
Operating rollers
Inconsistent measurement
method with the customers
Plates thickness reduction
of different steel types
Inconsistent measurement
positions
Thickness standard
Method
Operation of temper mill
Different flattening level thinning
for different steel types
Improper pressure adjustment
Rolling tension
Large thickness variation
of incoming materials
Confusion of
different plate types
Effect of covexity
of incoming plates
Effect of rolling
ingredients variation
Effect of hot
rolling plate wedge
Materials
Inconsistent annealing
properties
Over thickness
Figure 2. The cause and effect diagram of over thickness.
Table 2. C&E matrix of cold rolling plate thickness.
Rating of importance (1–10) 5 9
Key requirements Large variance Extra thickness
Process step Rating: 0–10 Total
1Thickness standard 8 5 85
2 Order 3 1 24
3Rolling parameters 3 9 96
4Stretching force 3 9 96
5 Plate temperature 3 3 42
6Compensating factor of thickness gauge 3 9 96
7Standard plates 1 9 86
8 Rolling oil 3342
9Power source 3 9 96
10 Oil residue on plate surface 3342
11 Measure position 6 2 58
12 Thickness reference revision 2 9 91
13 Thickness reference filled 2228
14 Contract requirement 5 3 52
15 Wedge-shaped raw material 9 3 72
16 Plate crown of raw material 4 3 47
17 Thickness of raw material 3 1 24
18 Ingredient Ni of raw material 9 1 54
19 Ingredient Cu of raw material 9 3 72
20 Ingredient Mo of raw material 9 3 72
21 Ingredient Cr of raw material 3 4 51
22 Ingredient Al of raw material 3124
23 Inspectors 3 3 42
24 Raw materials annealed 3 1 24
25 Flattening passes 9 3 72
26 Rolling passes 3 3 42
27 Rolling strain of final product pass 5 4 61
28 Rolling tension 1 3 32
29 Manual thickness measurement 3 9 96
30 Difference of rolling shift teams 6 3 57
31 Difference of rollers 6 3 57
32 Total rolling strain 3 4 24
Production Planning & Control 223
Table 3. FMEA of cold rolling plates.
Item
Potential failure
mode
Potential
effects of
failure
S
(Severity
rating) Potential causes
O
(Occurrence
rating)
Current
controls
D
(Detection
rating) RPN
Wedge-shaped
raw
material
Large variance Large
variation of
thickness
7 Incorrect wedge
control of hot
rolling raw
material
4N 4112
Ingredient Cr
of raw
material
Inaccurate
thickness
gauge
measurement
Thickness of
out
specification
6 Melting control 4 N 4 96
Ingredient Ni
of raw
material
Inaccurate
thickness
gauge
measurement
Thickness of
out
specification
6 Melting control 4 N 4 96
Ingredient Mo
of raw
material
Inaccurate
thickness
gauge
measurement
Thickness of
out
specification
6 Melting control 4 N 4 96
Ingredient Cu
of raw
material
Inaccurate
thickness
gauge
measurement
Thickness of
out
specification
6 Melting control 4 N 4 96
Rolling
parameters
Disunity Large
variation of
thickness
8 Failure to obey
design
6 3 144
Unreasonable
values
Extra
thickness
9 Design
parameters
insufficiency
4 Temporarily
set up
references
3 108
Rolling strain Non-standard Bad rolling
performance
5 Lack of quality
consciousness
6 Process
periodical
inspection
390
Rolling strain
of final
product
pass
Disunity Final product
thickness of
out
specification
3 Steel ingredient,
annealing and
process
7 N 6 126
Compensating
factor of
thickness
gauge
Not able to
find the best
value
Final product
thickness of
out
specification
7 Variance of
ingredients or
system error of
thickness gauge
3 N 6 126
Manual
thickness
measurement
Inaccurate
measurement
Inaccurate
actual
thickness
measurement
7 Incorrect
micrometre
calipers
5 Training 2 70
Power source Abnormal work Not scheduled
for
maintenance
or abnormal
9 Abnormal
problems such as
equipment
failure
1 Temporary
treatment
872
Rolling shift
teams
Different
operation
process
Poor
thickness
unity
4N 6 N 4 96
Rollers Different
system
Poor
thickness
unity
4 N 6 N 5 120
Standard plates Incorrect size Incorrect roller
thickness
control
10 Abnormal when
calibrating
1N 990
Flattening
passes
Non-standard Incorrect
thinning level
6 Strong
arbitrariness
5 Wide flow
for various
plate types
390
Stretching force Disunity Different
thinning level
6 Different raw
plate shape level
4 Focus on
improving
plate shape
248
(Continued)
224 M. Zhang et al.
There are 16 factors whose risk priority number
(RPN) is larger than or equal to 90. The cause of nine
factors, marked by bold type in Table 3, will be analysed
and improved by the statistical tools in the following
section. Another seven factors can be immediately
corrected through a simple and quick improvement
scheme. Then, a second FMEA of these seven factors is
analysed. Except that thickness standards need to be
coordinated with the design department, the RPN values
of the other six factors are all below 90, which are
shown in Table 4.
3.4.2. Analysis schemes
In this section, the effects of wedge-shaped raw material,
chemical ingredients, rolling shift teams and roller unit
Table 3. (Continued).
Item
Potential failure
mode
Potential
effects of
failure
S
(Severity
rating) Potential causes
O
(Occurrence
rating)
Current
controls
D
(Detection
rating) RPN
Thickness
standard
Many
personalised
standards
Poor process
control, order,
inspection and
judge
7 No standards
provided to
customers or
little standards
8N 2112
Measure
position
Incorrect
measurement
thickness
Not
conforming
with thickness
measured by
customer
5 Thickness
inconsistency
between the
middle and edge
of plate
4 C100
position
required
240
Thickness
reference
revision
Non-conformity
to the standard
Poor reference
thickness
6 Did not grasp
the points of
thickness
revision
5 Training and
check
390
Contract
requirement
Did not
distribute the
products
according to the
raw orders
Inconsistent
thickness
6 Handle non-
scheduled
products
3 Strengthen
equipment
inspection
236
Table 4. The improved FMEA of cold rolling process.
Items Failure mode Current status
Prior
RPN Measures taken S O D RPN
Rolling
parameters
Disunity Thickness specification is not
consistent with customer
requirements. Rolling parameters
are not fully carried out in practice
144 Parameters are redesigned. New
thickness standards and process needs
are well trained
823 48
Unreasonable 108 9 2 3 54
Thickness
standard
Many
personalised
standards
There are 1379 types of
thickness requirements and is
no unified standard
112 Based on customer requirements,
current standards and experience
in the industry, new thickness
standards are set down
772 98
Rolling
strain
Non-standard The relationship between raw
materials and finished products is
lack of standardisation
90 Based on the steel characteristics and
real production conditions, such
relationship is standardised
533 30
Standard
plates
Incorrect size In practice standard thicknesses of
some standard plates are not
precise
90 Each standard plate has to be
manually inspected to make sure
thickness is ok
10 0 9 0
Flattening
passes
Non-standard Thickness reduction amount is not
clear enough after flattening
process
90 After thorough learning of thickness
reduction amount of each process,
thickness unity is provided according
to steel types, thickness specification
and process requirements
623 36
Thickness
reference
revision
Non-
conformity to
the standard
Thickness revision concept is
misunderstood and not executed
consistently
90 Thickness reference is classified and
revised. Each inspector is well
trained
623 36
Production Planning & Control 225
on thickness yield control are analysed. Different tools
are used for different data types.
3.4.2.1. Effect of wedge-shaped raw materials. The
effect of wedge value of hot rolling plates on the thick-
ness of cold rolling plates is investigated here. Wedge is
a measure of the thickness at one plate edge as opposed
to the other edge. It may be expressed as absolute mea-
surements or as relative measurements. Here, absolute
measurements are used. In a hot rolling process, wedge
may be caused by rigidity of rolling mill, work piece
deviation, raw material wedge or uneven temperature.
Ten coils with target cold rolling plate thickness of 2.0
mm were randomly assigned to each nominal wedge val-
ues of 0.01, 0.04 and 0.07 mm. The thickness values of
cold rolling plates are shown in Table 5.
In the analysis, the hypothesis tested is as follows.
H
0
: there is no statistically significant thickness differ-
ence for different wedge values. H
1
: there is statistically
significant thickness difference for different wedge val-
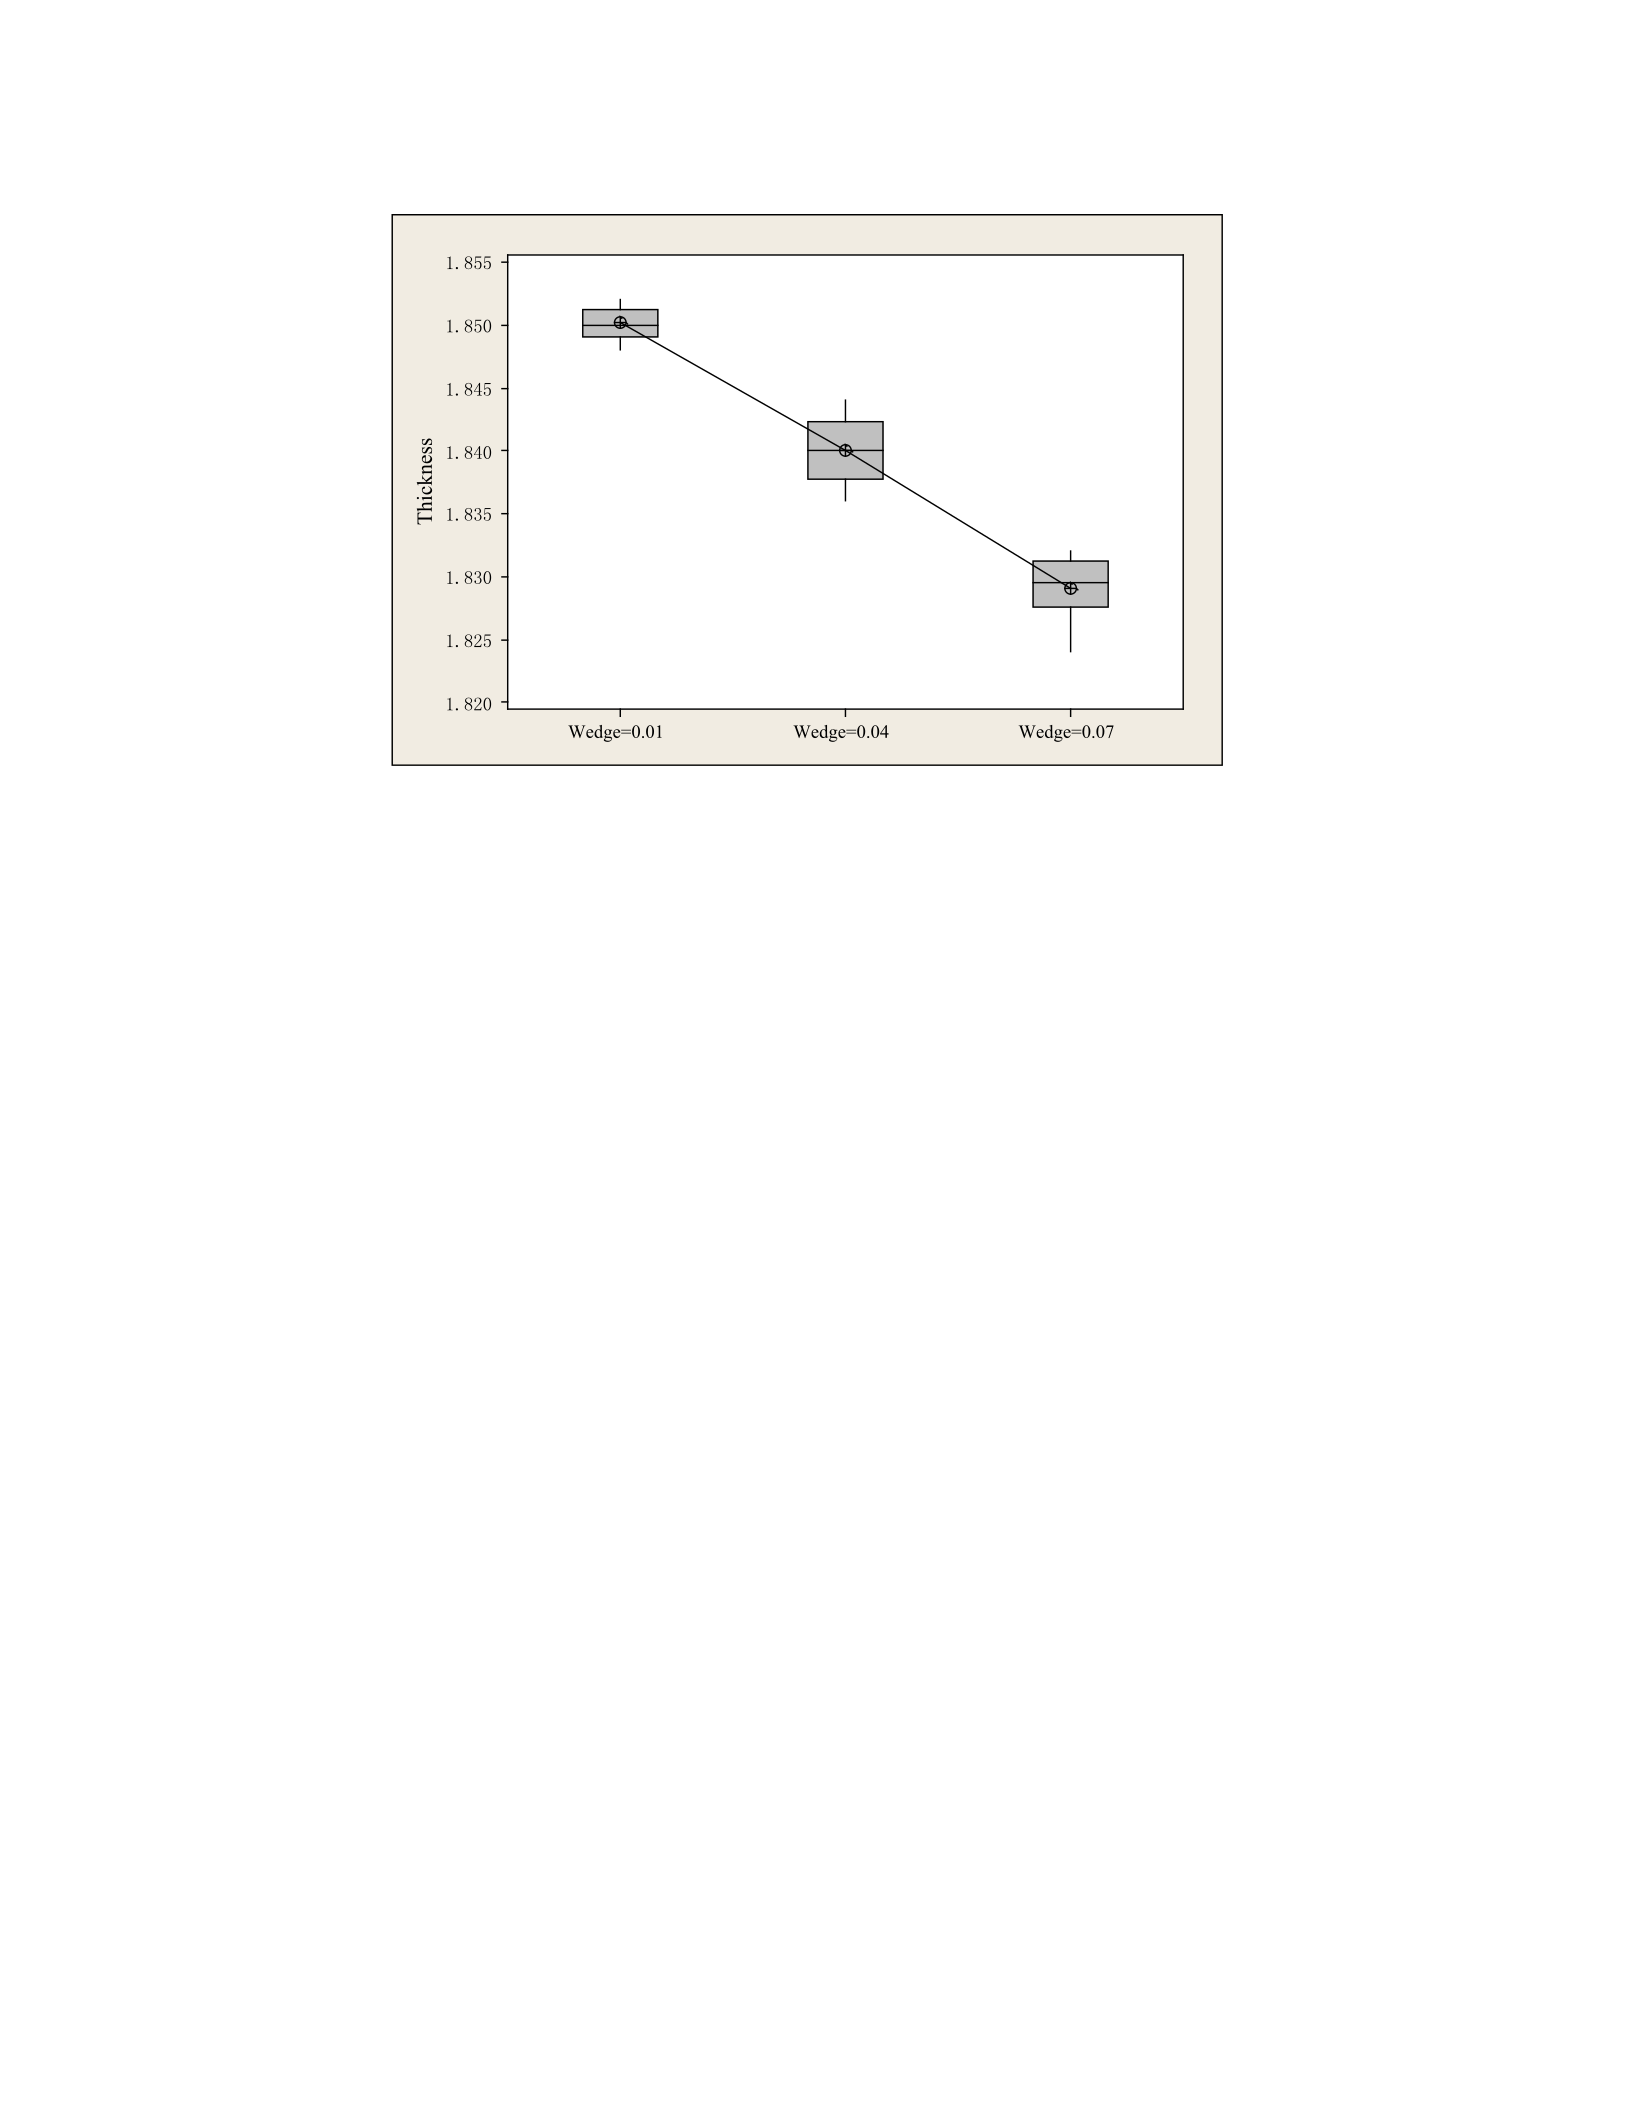
ues. One-way ANOVA is used and the results are shown
in Figure 3. Boxplots of thickness by wedge value are
shown in Figure 4. Because the resulting pvalue is vir-
tually zero, the null hypothesis is rejected, i.e. there are
statistically significant differences in the thickness for
different wedge values. Besides, when the wedge value
is 0.01 mm, the mean thickness is 1.85 mm, which is the
closest to target thickness 2.00 mm and the thickness
standard deviation is also the smallest. Therefore, the
wedge value of hot rolling plates should be 0.01 mm in
order to control the thickness variation of cold rolling
plates with target thickness 2.0 mm.
3.4.2.2. Effect of chemical ingredients Cr, Ni, Mo and Cu.
The addition of chemical ingredients makes the stainless
steel respond well to heat treatment, resulting in different
mechanical strengths, such as hardness and corrosion
resistance. However, there is variation in the chemical
ingredients due to measurement positions and the smelt-
ing processes. In this project, one type of stainless steel
with target thickness 2.00 mm contains 17–19% chro-
mium (Cr), 12–16% nickel (Ni), 1.2–2.5% copper (Cu)
and 1.5–2.5% molybdenum (Mo). The thickness is mea-
sured with the use of X-ray thickness gauge for 100
coils where 10 positions are chosen in each coil. Regres-
sion analysis between thickness and chemical ingredients
is shown in Figure 5. It can be seen from Figure 5that
the standard error is 0.0128 mm. The thickness variation
due to the ingredients can be controlled within ±3 ×
0.0128 mm, that is 0.0768 mm.
Moreover, the pvalues of ingredients Ni and Cr are
0.624 and 0.491, respectively, which are much larger
than 0.05. Thus, ingredients Ni and Cr do not signifi-
cantly affect the thickness. On the other hand, the pval-
ues of ingredients Cu and Mo are 0.015 and 0.004,
respectively, both being smaller than 0.05. Thus, there is
significant relationship between thickness and ingredients
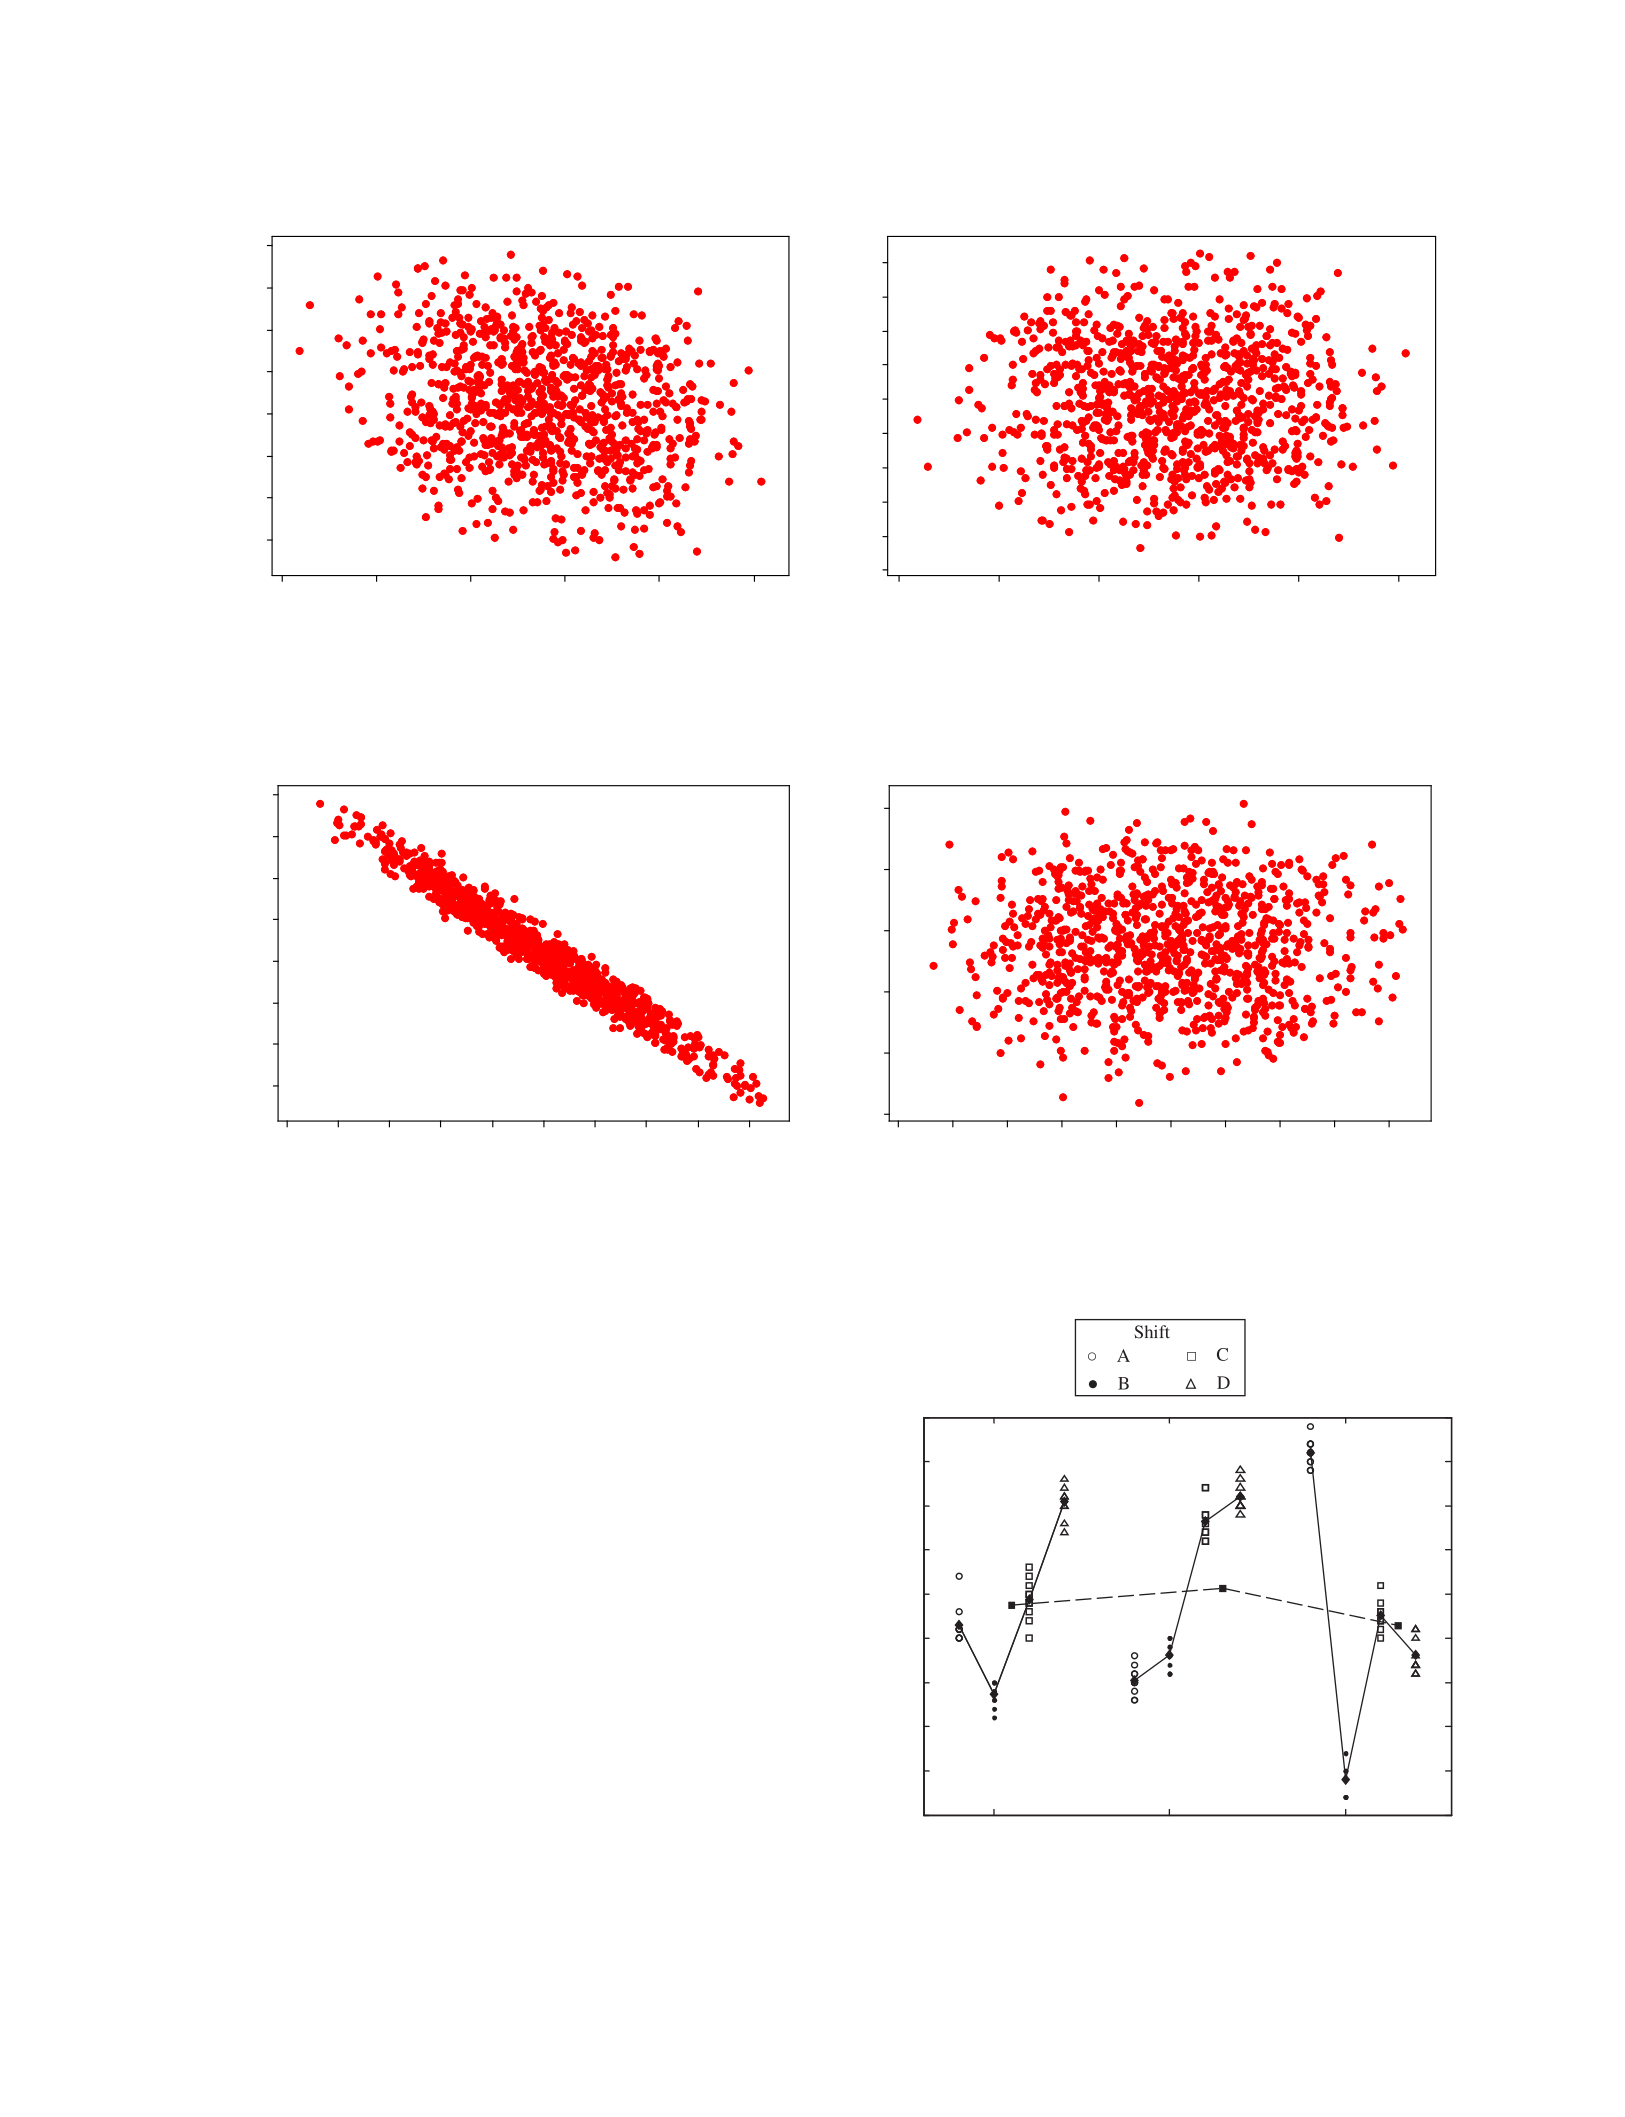
Cu and Mo. The scatter plots of thickness adjusted for
Cu vs. Mo adjusted for Cu are shown in Figure 6. Those
of thickness adjusted for Mo vs. Cu adjusted for Mo are
shown in Figure 7. Next, ingredients Ni and Cr are
deleted from the regression analysis. The regression
results are shown in Figure 8. The pvalues of ingredi-
ents Cu and Mo are 0.007 and 0.003, respectively, which
are smaller than 0.05. Thus, there is significant relation-
ship between thickness and ingredients Cu and Mo. In
practice, high-quality copper and molybdenum wires are
first mixed into the smelting furnace based on their lower
or middle specifications. The proportions of Cu and Mo
are measured at regular times. More wires may be used
in the smelting process.
One-way ANOVA: thickness versus Wedge
Source DF SS MS F P
Wedge 2 0.0022483 0.0011241 223.83 0.000
Error 27 0.0001356 0.0000050
Total 29 0.0023839
S = 0.002241 R-Sq = 94.31% R-Sq(adj) = 93.89%
Individual 95% CIs For Mean Based on Pooled StDev
Level N Mean StDev ---------+---------+---------+---------+
0.01 10 1.85020 0.00132 (-*-)
0.04 10 1.84000 0.00258 (--*-)
0.07 10 1.82900 0.00258 (-*-)
---------+---------+---------+---------+
1.8340 1.8410 1.8480 1.8550
Pooled StDev = 0.00224
Figure 3. Results of one-way ANOVA.
Table 5. Values of thickness with different wedges (unit: mm).
Wedge values 0.01 0.04 0.07
Thickness 1.850 1.840 1.830
1.852 1.842 1.828
1.851 1.843 1.830
1.852 1.841 1.826
1.850 1.844 1.824
1.849 1.838 1.828
1.851 1.839 1.831
1.849 1.837 1.832
1.848 1.836 1.829
1.850 1.840 1.832
226 M. Zhang et al.
3.4.2.3. Effect of rolling shift teams and roller unit.
Multi-vari analysis is used to analyse the effect of rolling
shift teams and roller unit on thickness. We chose three
rollers numbered 1#, 2# and 3# which are randomly
operated by four shifts named A, B, C and D. The thick-
nesses of ten coils are randomly measured for each shift
operating one roller. The thicknesses are shown in Fig-
ure 9. It can be seen that the thickness variation is
mainly caused by different shifts for each roller. How-
ever, the variation between different rollers is relatively
small. Thus, the front line workers should be well trained
according to operation instruction to guarantee produc-
tion consistency.
3.5. Improve
The main task in this step is to further analyse the effect
of rolling strain, compensating coefficient and rolling
parameter on the cold rolling plate thickness with the use
of design of experiments (DOE) (Box, Hunter, and Hun-
ter 2009). A full factorial design with three factors at two
levels (i.e. a 2
3
factorial design) with three centre points
is adopted. For confidential reason, the level selection for
each input variable and the raw data of experimental
design are not provided. The analysis is shown in Fig-
ure 10. It can be seen from Figure 10 that the three main
effects and the interaction between strain and compensat-
ing coefficients are significant. After deleting the insignif-
icant interactions in the model, the reduced model is
shown in Figure 11. There is no curvature and lack of fit
of the model. Residual analysis validates the appropriate-
ness of the model. As the curvature coefficient measures
the sum of the quadratic effects or strain and rolling
parameter, it is probably appropriate to add some star
points in the design in future investigations.
Optimisation is also used to find the best values of
strain, compensating coefficient and rolling parameter.
Based on the optimised values of these parameters, 20
coils of hot rolling plates with the target of thickness
2.0 mm are tested to observe if the actual thickness is
within the thickness specification limits. The thickness of
experimental coils falls in the confidence interval range,
which shows that the conclusions from the DOE analysis
are correct. The process parameters can be used in pro-
duction.
Figure 4. Boxplots of thickness by wedge value.
Regression Analysis: Thickness versus Cr, Ni, Mo, and Cu
The regression equation is
Thicknesses = 2.04 - 0.0111 Ni -0.00526 Cr – 0.0408 Cu – 0.197 Mo
Predictor Coef SE Coef T P
Constant 2.03570 0.18250 11.15 0.000
Ni -0.01112 0.02259 -0.49 0.624
Cr -0.00526 0.00759 -0.69 0.491
Cu -0.04083 0.01643 -2.49 0.015
Mo -0.19693 0.06560 -3.00 0.004
S = 0.0127556 R-S
q
= 80.9% R-S
q
(ad
j
) = 88.2%
Figure 5. Regression analysis between thickness and chemical
ingredients of Cr, Ni, Mo and Cu.
Production Planning & Control 227
2.22.01.81.61.41.2
2.03625
2.03600
2.03575
2.03550
2.03525
2.03500
2.03475
2.03450
Cu (%)
thickness (mm)
2.22.01.81.61.41.2
2.4
2.3
2.2
2.1
2.0
1.9
1.8
1.7
1.6
1.5
Cu (%)
Mo (%)
(a) (b)
Figure 6. (a) Thickness adjusted for Cu and (b) Mo adjusted for Cu.
1.5 1.6 1.7 1.8 1.9 2.0 2.1 2.2 2.3 2.4
2.03625
2.03600
2.03575
2.03550
2.03525
2.03500
2.03475
2.03450
Mo (%)
thickness (mm)
1.5 1.6 1.7 1.8 1.9 2.0 2.1 2.2 2.3 2.4
2.2
2.0
1.8
1.6
1.4
1.2
Mo (%)
Cu (%)
(a) (b)
Figure 7. (a) Thickness adjusted for Mo and (b) Cu adjusted for Mo.
Regression Analysis: Thickness versus Cu and Mo
The regression equation is
Thicknesses = 1.85 - 0.0443 Cu – 0.181 Mo
Predictor Coef SE Coef T P
Constant 1.85281 0.00212 875.77 0.000
Cu -0.04429 0.01592 -2.78 0.007
Mo -0.18053 0.05922 -3.05 0.003
S = 0.0126807 R-Sq = 80.1% R-Sq(ad
j
) = 88.8%
Figure 8. Regression analysis between thickness and chemical
ingredients of Cu and Mo.
1# 2# 3#
1.825
1.83
1.835
1.84
1.845
1.85
1.855
1.86
1.865
1.87
Roller
Thickness
Figure 9. Multi-vari chart of rollers and shifts.
228 M. Zhang et al.

3.6. Control
The significant key factors found in the measurement,
analysis and experiment steps are controlled through
control plans to sustain the effectiveness achieved
through the project. The aim is to keep the current thick-
ness level and prevent any quality deterioration. Such
actions are shown in Table 6.
The cold rolling coils are inspected periodically to
monitor the improved results. Here, an individual mov-
ing range control chart is used. The chart shows that the
thickness is in control.
The original thickness yield is only 68.90%. How-
ever, it reaches to 95.82% after the improvement of the
Six Sigma project. There is a significant increase in
thickness yield. Furthermore, the thickness yield is also
over the target value, that is 90%.
4. Economic benefit analysis
There were about 40 cold rolling coils with over-large
thickness per month before this project was carried out.
However, such number decreases to 5 coils per month
after improvement project. The cost of rolling and pick-
ling processes is 651RMB per ton, the cost reduction in
these two processes is 296,000RMB every month. Then
the cost reduction each year is 3552,000RMB. At the
same time, the loss due to quality rejections is
125,000RMB in 2009. Such loss after this project can be
reduced by about 72,000RMB each year. It is noted that
the application cost during this project mainly includes
the salaries of Black Belts and various team members,
amounting to about 10,000RMB. Thus, the economic
benefit is 3520,000RMB ($550,000) per year.
Factorial Fit: Thickness versus Strain, Compensation coefficient , Rolling parameter
Estimated Effects and Coefficients for Thickness (coded units)
Term Effect Coef SE Coef T P
Constant 1.84088 0.001061 1735.59 0.000
Strain 0.01125 0.00563 0.001061 5.30 0.034
Compensating coefficient 0.01575 0.00788 0.001061 7.42 0.018
Rolling parameter 0.01375 0.00687 0.001061 6.48 0.023
Strain*Compensating coefficient -0.00475 -0.00238 0.001061 -2.24 0.155
Strain*Rolling parameter 0.01125 0.00562 0.001061 5.30 0.034
Compensating coefficient* -0.00325 -0.00162 0.001061 -1.53 0.265
Rolling parameter
Curvature -0.00488 0.002031 -2.40 0.138
S = 0.003 R-Sq = 99.66% R-Sq(adj) = 95.43%
Analysis of Variance for Thickness (coded units)
Source DF Seq SS Adj SS Adj MS F P
Main Effects 3 0.00112738 0.00112738 0.00037579 41.75 0.023
2-Way Interactions 3 0.00031937 0.00031937 0.00010646 11.83 0.079
3-Way Interactions 1 0.00000613 0.00000613 0.00000613 0.68 0.496
Curvature 1 0.00005185 0.00005185 0.00005185 5.76 0.138
Residual Error 2 0.00001800 0.00001800 0.00000900
Pure Error 2 0.00001800 0.00001800 0.00000900
Total 10 0.00152273
Figure 10. Full factorial design analysis (full model).
Production Planning & Control 229
Factorial Fit: Thickness versus Strain, Compensation coefficient , Rolling parameter
Estimated Effects and Coefficients for Thickness (coded units)
Term Effect Coef SE Coef T P
Constant 1.83955 0.001468 1253.12 0.000
Strain 0.01125 0.00563 0.001721 3.27 0.017
Compensating coefficient 0.01575 0.00788 0.001721 4.57 0.004
Rolling parameter 0.01375 0.00688 0.001721 3.99 0.007
Strain*Rolling parameter 0.01125 0.00562 0.001721 3.27 0.017
S = 0.00286873 R-Sq = 98.82% R-Sq(adj) = 94.09%
Analysis of Variance for Thickness (coded units)
Source DF Seq SS Adj SS Adj MS F P
Main Effects 3 0.00112738 0.00112738 0.00037579 15.85 0.003
2-Way Interactions 1 0.00025312 0.00025312 0.00025312 10.68 0.017
Residual Error 6 0.00014223 0.00014223 0.00002370
Curvature 1 0.00005185 0.00005185 0.00005185 2.87 0.151
Lack of fit 3 0.00007238 0.00007238 0.00002413 2.68 0.283
Pure Error 2 0.00001800 0.00001800 0.00000900
Total 10 0.00152273
Figure 11. Factorial design analysis after optimisation (reduced model).
Table 6. The control plan of key factors.
No. Key factors Control style
Relative
unit
1 Process implementation of
rolling process
Check the implementation everyday Rolling
2 Implementation of thickness
inspection correctness
Check the thickness correctness everyday Inspection
3 Procedure of abnormal
thickness quality information
Thickness curve of abnormal coils has to be printed and recorded Rolling
4 Check and feedback of raw
material thickness control
Ten coils are sampled each month. The values of wedge and plate crown are
measured and fed back to the former process and management
Technique
5 Calibration of roller thickness
gauge
The compensating coefficient of thickness gauge for all kinds of steels has to be
calibrated each month
Electric
6 Thickness standard plates Based on the average level of steel ingredients, thickness standard plates are
calibrated in automated company
Technique
7 Rolling strain The corresponding specification between the final product thickness and raw
material is planned. The requirement for raw materials is reported each month
according to the contracts
Production
230 M. Zhang et al.

5. Discussion
The above project is just one example of the Black Belt
and Green Belt projects finished in Company T. From
2009 to 2011, Company T successfully conducted 475
projects which yielded 600 million RMB ($100,000,000)
hard savings. Twenty-one projects were selected as
national excellent Six Sigma projects by the China Asso-
ciation for Quality (CAQ). And Company T was
awarded as Excellent Company for Six Sigma Imple-
mentation by CAQ.
For a typical Chinese state-owned enterprise, Com-
pany T gained competitive advantages through Six
Sigma deployment in terms of quality improvement, cost
reduction and service enhancement. Through our investi-
gation into Company T, we found the following key suc-
cess factors for its Six Sigma implementation. All these
factors are almost the same as the research findings of
the previous literature (Coronado and Antony 2002; Lin-
derman et al. 2003; Kwak and Anbari 2006; Pandey
2007; Schroeder et al. 2008; Zu, Fredendall, and
Douglas 2008; Kumar, Antony, and Cho 2009;
Büyüközkan and Öztürkcan 2010; Zu, Robbins, and
Fredendall 2010; Brun 2011; Nair, Malhotra, and Ahire
2011; Parast 2011; Manville et al. 2012).
5.1. Strong support and involvement of top
management
Because Six Sigma is a top-down management activity,
commitment of top management becomes a key success-
ful factor of Six Sigma implementation. Commitment
does not only mean strong support by providing visible
resources for Six Sigma, but also means personal
involvement or participation in Six Sigma projects. In
Company T, top leaders act as the champions of Six
Sigma projects, which can make sure that each project
links to the company strategy and guarantees resources
input in the improvement process.
5.2. Career plan of belt employees
Six Sigma will never succeed without active participation
of Black Belts, Green Belts and Yellow Belts. To
motivate these belts employees, Company T designed a
career plan for them besides a monetary reward based on
the hard savings of the successful projects they finished.
Some managers are selected from the Black Belt or
Master Black Belt employees. Thus, Six Sigma manage-
ment can be carried out by the managers of each level in
the organisation, and become their daily work. The
continuous improvement mechanism and culture are
formed through continuously finding projects, defining
projects, managing projects and reviewing project
results.
5.3. Six Sigma infrastructure
Six Sigma infrastructure is one of the key elements to
maintain sustainable implementation of Six Sigma. In
Company T, a well-established infrastructure was estab-
lished at the very beginning when Six Sigma was
announced. A Six Sigma office was formed to be
responsible for Six Sigma project management. The head
of the office directly reported to the CEO. A five-year
Six Sigma implementation plan was drafted with specific
goals and tasks for each year. Also, a set of documents
was set up for Six Sigma project selection, project
review and financial results assessment.
5.4. Well-established action-learning training system
The uniqueness of Six Sigma training is based on prob-
lem-solving. Projects were selected before project team
members received Six Sigma training. Six Sigma training
is divided into different phases such as DMAIC or
DMADV and the training is in parallel with project exe-
cution. The belts employees are required to utilise what
they learned in the classroom to their projects with the
help of consultants. And Company T established a hier-
archy of training system targeted at champions, Black
Belts, Green Belts, Yellow Belts, staff members and
front line workers.
5.5. Information system
Information system can also be regarded as an important
element of infrastructure for Six Sigma companies. Suc-
cessful Six Sigma implementation needs reliable data
collection and analysis, which were poor before Six
Sigma was introduced into Company T. Along with Six
Sigma deployment, Company T also introduced MES
and ERP systems and upgraded its intranet system. The
well-established information system provides online data
collections. And Six Sigma office also developed its pro-
ject management system and put it on the website for
instant monitoring of project progress. Six Sigma project
success story sharing is also realised via intranet.
5.6. Six Sigma culture
For managers at each level, such idea as making use of
Six Sigma to promote operation performance and
increase company competition is sent out to each man-
agement area. All the managers know very well the core
of Six Sigma management and provide support and
resources to Six Sigma implementation. For engineers
and quality management employees, such idea as making
good use of data in Six Sigma implementation to achieve
quality management innovation is popularised. All of
them consciously use the theory and tools of Six Sigma
to raise the efficiency and quality management level of
Production Planning & Control 231
Company T. For the basic level employees, such idea as
using Six Sigma to reduce poor quality cost and increase
economic value added is practicable. Six Sigma manage-
ment becomes an essential part of their daily work.
5.7. Integration with other management methods
Other management methods such as Lean Production,
TPM, QC, ISO90001 and performance excellence model
were also introduced into Company T before Six Sigma
management. As mentioned above, Company T builds a
big Six Sigma umbrella at the corporate level which
includes Lean Production, TPM and others, since the
core value of these initiatives is continuous improve-
ment. The integration avoids the separations of continu-
ous improvement programmes with different names and
affiliated with different departments. And the integration
combines Six Sigma’s top-down strategy and the bot-
tom-up culture of lean to form critical mass for continu-
ous improvement.
6. Conclusions
It is well reported that many of the Top 500 corporations
in the world have implemented Six Sigma management
to improve their product and service quality. Systematic
and sustained applications of Six Sigma in China are,
however, not as widely known. This paper has outlined
the initiatives in the promotion of Six Sigma in one
famous steel organisation, namely Company T. A signifi-
cant Black Belt project at this company is also pre-
sented.
It can be appreciated from the accounts given here
that Six Sigma has become a prime mover in a com-
pany’s drive for global competitiveness, and the aligned
statistical tools in Six Sigma offer unprecedented oppor-
tunities for non-statisticians to integrate analytical tools
with technical problem-solving. What follows is a chang-
ing company culture that results from the behaviour of
employees and managers alike, ultimately realising the
goal of a learning organisation. Business leaders with
organisational capability, project management techniques
and habits of statistical diagnosis have emerged along
with Six Sigma management. In fact, they are the ones
that planted the seeds for reform and increased competi-
tiveness of the company –this has certainly more signifi-
cant and far-reaching implications than what many have
routinely seen in the DMAIC roadmap.
Funding
The authors were partially supported by the NSFC [grant
number 71002105], [grant number 71225006].
Notes on contributors
Min Zhang is an associate professor in the
College of Management and Economics,
Tianjin University. She received her MS in
materials engineering from Shandong
University, China, in 2003 and PhD in
management science and engineering from
Tianjin University, China, in 2006. Her
research interests focus on statistical quality
control, Six Sigma management and pro-
cess monitoring applications. She has published more than 20
papers in research journals, such as International Journal of
Production Economics, International Journal of Production
Research, Journal of Business Ethics, Total Quality Manage-
ment & Business Excellence, Quality and Reliability Engineer-
ing International et al.
Wei Wang is a quality engineer in Taiyuan Iron
& Steel Co., Ltd. He received his master of
engineering from the Tianjin University,
China, in 2011. His research interests focus on
Six Sigma management and quality control.
Thong Ngee Goh is a professor in the
Department of Industrial and Systems Engi-
neering at the National University of Singa-
pore. He has published some 300 peer-
reviewed research papers and five advanced
books related to Quality Engineering and
Management. He is currently on the edito-
rial boards of more than 10 research jour-
nals. His recent international honours and
competitive awards include: IAQ Inaugural Masing Medal in
2006 (for the book ‘Six Sigma: Advanced Tools for Black
Belts and Master Black Belts’, Wiley, UK), ASQ Statistics
Division William G Hunter award in 2007 and ASQ Eugene L
Grant Medal in 2012. He is one of the only two persons in the
world to have received both the Hunter the Grant awards from
ASQ, in the 50-year history of the Grant Medal. His research
interests focus on statistical process control, design of experi-
ment and Six Sigma management.
Zhen He is a professor in the College of
Management and Economics, Tianjin Uni-
versity. He is also the Six Sigma consultant
of Company T. He is the recipient of Out-
standing Research Young Scholar Award of
the National Natural Science Foundation of
China. He has published more than 100
papers and co-authored five books. He is
the chairman of the Six Sigma Expert
Steering Committee of China Association for Quality. His
research interests focus on quality management, statistical qual-
ity control, DOE and Six Sigma management.
232 M. Zhang et al.

References
Aboelmaged, M. G. 2010. “Six Sigma Quality: A Structured
Review and Implications for Future Research.”International
Journal of Quality and Reliability Management 27 (3): 268–317.
Aksoy, B., and Â. Y. Orbak. 2009. “Reducing the Quantity of
Reworked Parts in a Robotic Arc Welding Process.”Quality
and Reliability Engineering International 25: 495–512.
Anand, R. B., S. K. Shukla, A. Ghorpade, M. K. Tiwari, and
R. Shankar. 2007. “Six Sigma-based Approach to Optimize
Deep Drawing Operation Variables.”International Journal of
Production Research 45 (10): 2365–2385.
Antony, J., E. V. Gijo, and S. J. Childe. 2012. “Case Study in
Six Sigma Methodology: Manufacturing Quality Improve-
ment and Guidance for Managers.”Production Planning and
Control 23 (8): 624–640.
Bañuelas, R., J. Antony, and M. Brace. 2005. “An Application
of Six Sigma to Reduce Waste.”Quality and Reliability
Engineering International 21: 553–570.
Bilgen, B., and M. Sen. 2012. “Project Selection through Fuzzy
Analytic Hierarchy Process and a Case Study on Six Sigma
Implementation in an Automotive Industry.”Production
Planning and Control 23 (1): 2–25.
Box, G. E. P., J. S. Hunter, and W. G. Hunter. 2009. Statistics
for Experimenters: Design, Innovation and Discovery. 2nd
ed. Hoboken, NJ: John Wiley.
Brun, A. 2011. “Critical Success Factors of Six Sigma Imple-
mentations in Italian Companies.”International Journal of
Production Economics 131: 158–164.
Büyüközkan, G., and D. Öztürkcan. 2010. “An Integrated
Analytic Approach for Six Sigma Project Selection.”Expert
Systems with Applications 37: 5835–5847.
Chakravorty, S. S. 2009. “Six Sigma Programs: An Implemen-
tation Model.”International Journal of Production Econom-
ics 119: 1–16.
Chen, H. C., K. S. Chen, T. L. Chang, and C. H. Hsu. 2010.
“An Application of Six Sigma Methodology to Enhance
Leisure Service Quality.”Quality and Quantity 44 (6):
1151–1164.
Chen, M. N., and J. J. Lyu. 2009. “A Lean Six-Sigma
Approach to Touch Panel Quality Improvement.”Production
Planning and Control 20 (5): 445–454.
Christiansen, Ó. 2011. “Rethinking ‘Quality’by Classic
Grounded Theory.”International Journal of Quality and Ser-
vice Sciences 3 (2): 199–210.
Coronado, R. B., and J. Antony. 2002. “Critical Success Fac-
tors for the Successful Implementation of Six Sigma Projects
in Organisations.”The TQM Magazine 14 (2): 92–99.
Deming, W. E. 1993. The New Economics –For Industry, Gov-
ernment, Education. Cambridge: Massachusetts Institute of
Technology.
Desai, D. A. 2006. “Improving Customer Delivery Commit-
ments the Six Sigma Way: Case Study of an Indian Small
Scale Industry.”International Journal of Six Sigma and
Competitive Advantage 2 (1): 23–47.
El Haouzi, H., J. F. Petin, and A. Thomas. 2009. “Design and
Validation of a Product-driven Control System Based on a
Six Sigma Methodology and Discrete Event Simulation.”
Production Planning and Control 20 (6): 510–524.
Ghosh, S., and J. Maiti. 2012. “Data Mining Driven DMAIC
Framework for Improving Foundry Quality –A Case Study.”
Production Planning and Control. Available Online,
doi:10.1080/09537287.2012.709642.
Gijo, E. V., J. Scaria, and J. Antony. 2011. “Application of Six
Sigma Methodology to Reduce Defects of a Grinding Pro-
cess.”Quality and Reliability Engineering International 27
(8): 1221–1234.
Jou, Y. T., C. H. Chen, C. H. Hwang, W. T. Lin, and S. J.
Huang. 2010. “A Study on the Improvements of New Prod-
uct Development Procedure Performance –An Application
of Design for Six Sigma in a Semi-conductor Equipment
Manufacturer.”International Journal of Production Research
48 (19): 5573–5591.
Kumar, M., J. Antony, and B. R. Cho. 2009. “Project Selection
and Its Impact on the Successful Deployment of Six Sigma.”
Business Process Management Journal 15 (5): 669–686.
Kumar, M., J. Antony, R. K. Singh, M. K. Tiwari, and D. Perry.
2006. “Implementing the Lean Sigma Framework in an
Indian SME: A Case Study.”Production Planning and Con-
trol 17 (4): 407–423.
Kwak, Y. H., and F. T. Anbari. 2006. “Benefits, Obstacles, and
Future of Six Sigma Approach.”Technovation 26: 708–715.
Li, S., C. Wu, D. C. Yen, and M. Lee. 2011. “Improving the Effi-
ciency of IT Help-desk Service by Six Sigma Management
Methodology (DMAIC) –A Case Study of C Company.”Pro-
duction Planning and Control 22 (7): 612–627.
Lin, C. J., F. F. Chen, H. Wan, Y. M. Chen, and G. Kuriger.
2013. “Continuous Improvement of Knowledge Management
Systems Using Six Sigma Methodology.”Robotics and Com-
puter-Integrated Manufacturing 29 (3): 95–103.
Linderman, K., R. G. Schroeder, S. Zaheer, and A. S. Choo.
2003. “Six Sigma: A Goal-theoretic Perspective.”Journal of
Operations Management 21: 193–203.
Lo, W. C., K. M. Tsai, and C. Y. Hsieh. 2009. “Six Sigma
Approach to Improve Surface Precision of Optical Lenses in
the Injection-molding Process.”The International Journal of
Advanced Manufacturing Technology 41 (9–10): 885–896.
Manville, G., R. Greatbanks, R. Krishnasamy, and D. W.
Parker. 2012. “Critical Success Factors for Lean Six Sigma
Programs: A View from Middle Management.”International
Journal of Quality and Reliability Management 29 (1): 7–20.
Nair, A., M. K. Malhotra, and S. L. Ahire. 2011. “Toward a
Theory of Managing Context in Six Sigma Process-improve-
ment Projects: An Action Research Investigation.”Journal
of Operations Management 29: 529–548.
Pandey, A. 2007. “Strategically Focused Training in Six Sigma
Way: A Case Study.”Journal of European Industrial Train-
ing 31 (2): 145–162.
Parast, M. M. 2011. “The Effect of Six Sigma Projects on
Innovation and Firm Performance.”International Journal of
Project Management 29 (1): 45–55.
Schroeder, R. G., K. Linderman, C. Liedtke, and A. S. Choo.
2008. “Six Sigma: Definition and Underlying Theory.”
Journal of Operations Management 26: 536–554.
Su, C. T., and C. J. Chou. 2008. “A Systematic Methodology
for the Creation of Six Sigma Projects: A Case Study of
Semiconductor Foundry.”Expert Systems with Applications
34: 2693–2703.
Production Planning & Control 233

Tanik, M., and A. Sen. 2012. “A Six Sigma Case Study in a Large-
scale Automotive Supplier Company in Turkey.”Total Quality
Management and Business Excellence 23 (3–4): 343–358.
Yang, T., and C. H. Hsieh. 2009. “Six-Sigma Project Selection
Using National Quality Award Criteria and Delphi Fuzzy
Multiple Criteria Decision-making Method.”Expert Systems
with Applications 36: 7594–7603.
Zu, X., L. D. Fredendall, and T. J. Douglas. 2008. “The
Evolving Theory of Quality Management: The Role of Six
Sigma.”Journal of Operations Management 26: 630–650.
Zu, X., T. L. Robbins, and L. D. Fredendall. 2010. “Mapping
the Critical Links between Organizational Culture and TQM/
Six Sigma Practices.”International Journal of Production
Economics 123: 86–106.
234 M. Zhang et al.

1
Abstract
I. Case study reporting is a complex task that requires the careful formatting and
presentation of relevant evidence.
Introduction
I. Case study results reporting is an intricate task requiring careful formatting and
presentation of relevant evidence (Alpi & Evans, 2019).
Case Study Report Audience and Reporting Methodology
I. Different case studies are conducted to address the needs of different potential audiences
(Yin, 2018).
II. According to Yin (2018), a case study investigation can have several potential audiences.
III. Yin (2018) discusses six approaches to composing a case study report.
Visual and Textual Materials of a Case Study Report
I. Case study data can be effectively reported by using a combination of visual and textual
materials (Midway, 2020).
II. Visual materials are used in reports to support textual materials (Midway, 2020).
Reporting Evidence: Striking the Balance
I. According to Kharasch et al. (2020), scientific studies are peer-reviewed by experts with
similar competencies by the researchers to ensure that the studies present quality findings
and reported findings are valid, among other things.

2
II. Peer review is one reason why a researcher should provide adequate evidence to help
experts evaluate their findings and conclusion (Kharasch et al., 2020).
Multiple-Case Case Study with Lean Six Sigma
I. The design multiple-case case study regards implementing the six sigma method in Hon
Hai Precision Industry Co., Ltd’s (Foxconn) manufacturing plants in China, Taiwan, and
Thailand.
II. Data relevant to the evaluation of process performance after implementing the lean six
sigma method will be collected to help determine whether the method is efficient in
improving Faxconn factories’ processes or otherwise.
Conclusion
I. Case study researchers have to be thorough when preparing the final case study report to
ensure that the report presents all necessary evidence to justify findings and conclusions
and caters to the needs of potential audiences.
1
Multiple-Case Case Study
Name
Institution Affiliation
Course Name
Instructor
Date
Author Note
Lakisha Lane
By submitting this assignment, I attest this submission represents my own work, and not
that of another student, scholar, or internet source. I understand I am responsible for
knowing and correctly utilizing referencing and bibliographical guidelines. I have not
submitted this work for any other class. Correspondence concerning this article should be
addressed to Lakisha Lane.
Email: lllane@liberty.edu

2
Abstract
Case study reporting is a complex task that requires the careful formatting and presentation of
relevant evidence. Case study report potential audiences include academics, policymakers,
sponsors or funders, committees, community leaders, practitioners, and relevant professionals.
Approaches used to report case study findings are the linear-analytic, comparative structure,
chronological structure, theory-building, suspense, and the unsequenced methods. Visual and
textual materials need to be effectively utilized in a case study report to improve the report’s
quality. The appropriate amount of evidence that a case study researcher should provide readers
is the evidence necessary to adequately evaluate all of the researchers’ findings and conclusions
regarding the research phenomenon. The Bible prohibits a Christian from lying. Colossians 3:9
states, “Lie not one to another, seeing that ye have put off the old man with his deeds” (King
James Bible, 2017). A Christian case study researcher ought not to lie in their case study report
as such would be unchristian.
Keywords: multiple-case case study, report audience, reporting methodology, visual
material, textual material

3
Introduction
Case study results reporting is an intricate task requiring careful formatting and
presentation of relevant evidence (Alpi & Evans, 2019). Evidence reporting needs to be guided
by a study’s target audience (Yin, 2018). Failure to consider the audience in evidence reporting
can result in a report that is inaccessible to the target audience or one that does not satisfy the
target audience's needs (Yin, 2018). A case study researcher has to determine the best visual aids
to use to help easily communicate research findings to the study’s intended audience (Yin, 2018).
Adequate evidence must be reported to aid readers to effectively assess a case study and its
findings (Yin, 2018). This discussion explains different case study audiences, reporting
methodologies, the textual and visual material that can be utilized in a case study report, and the
right amount of evidence to provide readers to help them understand a study. The discussion also
presents a sample multiple-case case study design aimed at evaluating the execution of the lean
six sigma methodology in an organization.
Case Study Report Audience and Reporting Methodology
Different case studies are conducted to address the needs of different potential audiences
(Yin, 2018). To ensure that a case study report suits the target audience's needs and can be easily
read by the audience, researchers have to carefully consider their reporting methodology vis-à-
vis the target audience (Shulman et al., 2020). Failure to make such consideration would result in
a case study report that either fails to suit target audience needs or is inaccessible to the target
audience (Shulman et al., 2020). Getting other people to review draft case study reports can help
improve the report (Yin, 2018). Thus, ensuring that it effectively presents case study evidence
vis-à-vis the target audience.

4
Case Study Report Audience
According to Yin (2018), a case study investigation can have several potential audiences.
One potential audience for a case study is an academic audience. Academics may read through a
case study report to understand a research phenomenon or identify the need for further research,
among other things. Policymakers are other potential audiences for a case study report.
Policymakers would be largely interested in a case study's contribution to policy evaluation or
policy-related decision-making (Uneke et al., 2018). Research sponsors or funders are other
potential case study audiences (Yin, 2018). For example, a business organization may sponsor or
fund a case study to help improve its processes or operations. Other potential audiences include
thesis committees, community leaders, practitioners, and relevant professionals (Yin, 2018). The
diverse range of potential audiences’ mean that case study researchers must tailor their reports to
cater to potential audiences’ needs (Yin, 2018).
Reporting Methodology
Yin (2018) discusses six approaches to composing a case study report. One of the
approaches is the linear-analytic method. The reporting method involves linearly writing
research report subtopics. A researcher begins with the problem or issue subtopic then proceeds
to the sequentially discuss the subtopics that are part of the analytic reporting approach. Another
reporting methodology is the comparative structure method. The approach involves comparing
differing explanations or descriptions in a report. The third methodology is the chronological
structure method. It involves presenting case study evidence in chronological order. Another
reporting approach open to case study researchers is the theory-building approach. The theory-
building approach involves presenting a theoretical argument in each report section. The fifth
reporting methodology is the suspense approach. It involves discussing the main outcome in a

5
report’s initial section or chapter and discussing explanations for the main outcome in the later
chapters. The sixth reporting approach available to case study researchers is the unsequenced
method which involves the report does not follow any particular sequence. When the sixth
approach is used, report sections or chapters carry no particular importance.
Visual and Textual Materials of a Case Study Report
Case study data can be effectively reported by using a combination of visual and textual
materials (Midway, 2020). Visual materials are used to visualize data (Midway, 2020). Data
visualization concerns the communication of data or information through the utilization of visual
objects (Midway, 2020). One of the visual materials or objects used to report case study data is
tables (Midway, 2020). Textual or numerical case study data or information can be formatted in
the form of a table to help ease the reading and understanding the data or information. Another
visualization object is graphs (Midway, 2020). Research data can be plotted into graphs for
easier reading and understanding (Midway, 2020). The third visual method is charting (Midway,
2020). Pie charts, bar charts, and line charts are examples of charts that can be used to easily
report case study data or information (Midway, 2020). A map is another visual material that can
be used to report case study data or information. (Midway, 2020) The utilization of visuals helps
make case study reports accessible to potential audiences (Midway, 2020).
Visual materials are used in reports to support textual materials (Midway, 2020). Textual
materials regard words, sentences, and paragraphs used to deliver certain information (Midway,
2020). According to Rashid et al. (2019), case study findings have to be explained thoroughly
using effective sentences and paragraphs. Textual materials are necessary in all case study report
sections. Text is needed to present the introduction, review relevant literature, methods used to
conduct the case study, findings, discussion, and conclusion, among other components of a case

6
study report (Yin, 2018). Textual materials are also needed to support visual objects or explain
the visual objects (Midway, 2020). The potential audience must inform the textual materials used
in a case study report to ensure that the report is accessible to the audience (Yin, 2018).
Reporting Evidence: Striking the Balance
According to Kharasch et al. (2020), scientific studies are peer-reviewed by experts with
similar competencies by the researchers to ensure that the studies present quality findings and
reported findings are valid, among other things. For a study to be effectively peer-reviewed, a
researcher has to clearly explain the method that they used to conduct the study, the evidence
collected and analyzed, and how they arrived at their conclusions based on analyzed evidence.
Thus, a researcher does not need to only prove to peer-reviewers how they arrived at their
conclusion. They also have to provide adequate evidence to help the reviewers arrive at their
conclusion regarding a research phenomenon. The appropriate amount of evidence that a case
study researcher should provide readers is the evidence necessary to adequately evaluate all of
the researchers’ findings and conclusions regarding the research phenomenon. Without adequate
evidence to evaluate all findings and conclusions, a reader cannot reliably arrive at their
conclusion regarding a particular case study.
Peer review is one reason why a researcher should provide adequate evidence to help
experts evaluate their findings and conclusion (Kharasch et al., 2020). Providing adequate
evidence to evaluate a case study's findings and conclusion and for the readers to come to their
conclusions is important as it would help prevent a study from spreading biased findings and
conclusions to readers (Kharasch et al., 2020). If a study’s findings and conclusions are biased
and there is no adequate evidence provided in the study report that can help identify the bias,
readers may accept the biased findings and conclusions and have a distorted image of reality

7
(Kharasch et al., 2020). A case study researcher should provide evidence that will help support
their findings and conclusions and also help readers evaluate their findings and conclusions.
Multiple-Case Case Study with Lean Six Sigma
The design multiple-case case study regards implementing the six sigma method in Hon
Hai Precision Industry Co., Ltd’s (Foxconn) manufacturing plants in China, Taiwan, and
Thailand. Foxconn is a manufacturing services provider with factories in countries in Asia,
Europe, and South America (Foxconn, n.d.). Foxconn is well-known for manufacturing iPhone
smartphones on behalf of Apple (Foxconn, n.d.). Foxconn aims to improve manufacturing
processes in its different factories worldwide. A lot of waste has been resulting from the
processes. Foxconn has decided to test the lean six sigma method in improving process
performance and reducing waste in three of its factories situated in China, Taiwan, and Thailand.
The three factories are the units of analysis. The multiple-case case study aims to evaluate the
performance of the lean six sigma method in Faxconn's China, Taiwan, and Thailand factories.
Data relevant to the evaluation of process performance after implementing the lean six
sigma method will be collected to help determine whether the method is efficient in improving
Faxconn factories’ processes or otherwise. Evidence sources for the study will include
interviews, documents, and archival records. The evidence from each case will first be analyzed
to evaluate lean six sigma's impact on the factories processes. Cross-case analysis and synthesis
will be conducted for all three cases to help evaluate whether the lean six sigma method is
effective in the three factories or otherwise. The cross-case analysis and synthesis will help
Foxconn determine whether there are factory-specific factors vital to the successful
implementation of the lean six sigma method in different factories. The case study will help
effectively implement lean six sigma on all Foxconn's factories if the company opts for the same.

8
Conclusion
Case study researchers have to be thorough when preparing the final case study report to
ensure that the report presents all necessary evidence to justify findings and conclusions and
caters to the needs of potential audiences. Case study report potential audiences include
academics, policymakers, sponsors or funders, committees, community leaders, practitioners,
and relevant professionals. The utilization of the relevant reporting methodology would help
effectively report research findings. Case study researchers must provide enough evidence for
readers to draw independent conclusions regarding their studies. One biblical teaching that ought
to guide case study reporting is honesty. Honesty regards being truthful. The Bible prohibits a
Christian from lying. Colossians 3:9 states, “Lie not one to another, seeing that ye have put off
the old man with his deeds” (King James Bible, 2017). A Christian case study researcher ought
not to lie in their case study report as such would be unchristian. Lying would also be contrary to
research ethics.
9
References
Alpi, K. M., & Evans, J. J. (2019). Distinguishing case study as a research method from case
reports as a publication type. Journal of the Medical Library Association: JMLA, 107(1),
1-5. https://doi.org/10.5195/jmla.2019.615
Foxconn. (n.d.). About Hon Hai. https://www.foxconn.com/en-us/about/group-profile
https://doi.org/10.1080/09537287.2014.891058
Kharasch, E., Avram, M., Clark, J., Davidson, A., Houle, T., & Levy, J. et al. (2020). Peer
Review Matters: Research Quality and the Public Trust. Anesthesiology, 134(1), 1-6.
https://doi.org/10.1097/aln.0000000000003608
King James Bible. (2017). King James Bible
Online. https://www.kingjamesbibleonline.org/Colossians-3-9/ (Original work published
1769)
Midway, S. (2020). Principles of Effective Data Visualization. Patterns, 1(9), 100141.
https://doi.org/10.1016/j.patter.2020.100141
Rashid, Y., Rashid, A., Warraich, M. A., Sabir, S. S., & Waseem, A. (2019). Case study method:
A step-by-step guide for business researchers. International Journal of Qualitative
Methods, 18, 1609406919862424. https://doi.org/10.1177/1609406919862424
Shulman, H. C., Dixon, G. N., Bullock, O. M., & Colón Amill, D. (2020). The effects of jargon
on processing fluency, self-perceptions, and scientific engagement. Journal of Language
and Social Psychology, 39(5-6), 579-597. https://doi.org/10.1177/0261927X20902177
Uneke, C. J., Ezeoha, A. E., Uro-Chukwu, H. C., Ezeonu, C. T., & Igboji, J. (2018). Promoting
researchers and policy-makers collaboration in evidence-informed policy-making in
Nigeria: outcome of a two-way secondment model between university and health